Custom Hot Forging Services
Get customized hot forging tooling, controlled heat treatment, and in-house CNC machining on one purchase order.
- Closed-die, open-die, and ring-rolled hot forging at 1200–2370 °F (650–1300 °C)
- Turnkey integration: multi-impression dies, flash trimming, CNC machining & 40+ finishes
- Scalable from 10 prototypes to 10M+ production parts
- 650–1300 °C1200–2370 °F hot forming
- 0.1 – 50 kg0.22 – 110 lbs net forged weight
- BS EN 10243-1Class F fine die tolerances
- IATF 16949:201624-hr quote & free DFM review
Customized Hot Forging Tooling
Before cutting your impression dies, our R&D engineering team reviews your 3D CAD and 2D drawings inside 24 hours
- Single-Source Die & CNC Fixture Ownership: Meco designs both the hot forging die and the CNC machining fixture in-house
- Controlled Heat Treatment & Finishing: Direct transfer from the forging press and trim die to in-house normalising, quenching & tempering, or T6 aging and surface finishing
- Low-Volume Bridge (<200 Pieces): We CNC-machine prototypes from solid forged bar stock in 1–2 weeks while your production hot forging dies are built (6–12 weeks)
Hot Forged Metals, Die Operations & Heat Treatment
Net weight capacity: 0.1 to 50 kg (0.22 to 110 lbs). All billets ship with EN 10204 3.1 mill certificates. Switch tabs below to view alloy forging temperatures or die and post-forging operations.
| Metal Family | Stocked Grades | Forging Temp | Heat Treatment & Typical Hot Forged Parts |
|---|---|---|---|
| Carbon Steel | 1045, 1035, 1020 | 1100–1250 °C (2010–2280 °F) | Normalise, quench & temper; forged shafts, axles, levers, yokes, and automotive wheel hubs |
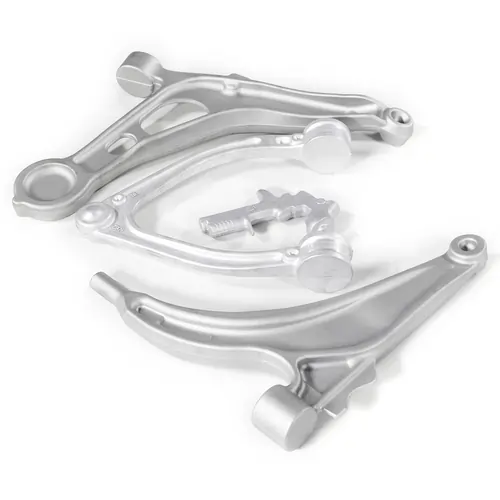
| Alloy Steel | 4140, 4340, 42CrMo | 1100–1230 °C (2010–2250 °F) | Quench & temper for shock load; steering knuckles, control arms, gear blanks, track links & bucket teeth |
| Stainless Steel | 304, 316, 17-4PH | 1100–1200 °C (2010–2190 °F) | Solution anneal & age harden; high-pressure industrial valve bodies, flanges, pump shafts, couplings |
| Aluminum | 6061, 6082, 7075, 2024 | 380–480 °C (715–900 °F) | T6 solution & age hardening; lightweight aerospace structural fittings, brackets, suspension links |
| Brass & Copper | C377, C360, C464; C110, C101 | 650–850 °C (1200–1560 °F) | Stress relieve / anneal; hot forged valve bodies, manifold blocks, appliance fittings, heavy power lugs |
| Operation | Compatible Forgings | Equipment Capability & Functional Benefit |
|---|---|---|
| Multi-Impression Dies & Trimming | Closed-Die Forgings | Pre-form blocker and finisher cavities, automated flash trimming, piercing, and coining (See Capabilities) |
| Controlled Heat Treatment | Carbon, Alloy, SS, Aluminum | In-house normalising, quenching & tempering, solution annealing, and T6 aging (Explore Heat Treatment) |
| Precision CNC Machining | All Hot Forged Blanks | 3/4/5-axis CNC milling and CNC turning of critical bores, threads, and sealing faces to ±0.01 mm (±0.0004″) |
| Descaling & Surface Finishing | All Hot Forged Metals | Shot blasting, zinc plating, hot-dip galvanizing, Type II/III anodizing, E-coat, and powder coating (40+ Finishes) |
Closed-Die vs. Open-Die Hot Forging vs. Cold Forging & Casting
Compare die configuration, forming temperature, net part weight, and annual volume economics across our custom metal forging and casting processes.
| Comparison Factor | Closed-Die Hot Forging | Open-Die & Ring Rolling | Cold Forging | Metal Casting |
|---|---|---|---|---|
| Best For | Complex 3D structural parts, knuckles, yokes, gear blanks Max Toughness | Large shafts, seamless rings, blocks & low-volume blanks No Custom Die | Small high-volume fasteners, pins & bushings Lowest Unit Cost | Intricate internal cavities & thin-walled housings |
| Equipment & Die Setup | Multi-cavity impression dies (blocker/finisher) + flash trim press | Flat/V-dies, mandrels & ring rolling mills | Multi-station cold headers & progressive dies | Bonded sand patterns or permanent steel dies |
| Temp & Net Weight | 650–1300 °C | 0.1–50 kg (0.22–110 lbs) | 650–1300 °C | 5–50 kg (11–110 lbs) | Ambient–200 °C | 0.01–5 kg (0.02–11 lbs) | Molten pour | 1 g–100 kg (0.002–220 lbs) |
| As-Formed Tolerance | BS EN 10243-1 Class F (0.6–1.3 mm) & ASTM B247 | 3 to 6 mm allowance (CNC machined after) | ±0.05 to 0.2 mm (bright scale-free surface) | CT7–CT10 or NADCA ±0.010″ |
| Ideal Annual Volume | 1,000 to 1,000,000+ parts/yr | 1 to 500 parts/yr | 50,000 to 10,000,000+ parts/yr | 50 (sand) to 1M+ (die casting) |
| Dedicated Service | Current Service | Explore Forging Blanks → | Explore Cold Forging → | Explore Custom Casting → |
Ready to Start Your Custom Hot Forging Project?
Upload your 3D CAD and 2D drawings for itemised die and piece pricing, signed NDA protection, and a free DFM review inside 24 hours.
Hot Forging Tolerances (BS EN 10243-1 & ASTM B247)
Compare our published as-forged drop forging tolerances against our in-house ±0.01 mm (±0.0004″) CNC finish-machining capabilities.
| Forged Feature | Steel Hot Drop Forging | Aluminum Hot Forging | Post-Forging CNC Machined | CMM Verification |
|---|---|---|---|---|
| Inside-Die Dimensions | 0.6 to 1.3 mm (Class F Fine) | Per ASTM B247 / drawing | ±0.01 mm (±0.0004″) | ±0.002 mm (±0.00008″) |
| Across Parting Line (Die Closure) | +0.6 / −0.3 mm (up to 0.5 kg) | +0.80 / −0.40 mm (up to 0.5 kg) | ±0.01 mm flatness/datum | ±0.002 mm (±0.00008″) |
| Bores, Shafts & Bearing Fits | Pre-formed or solid boss | Pre-formed or solid boss | ±0.005 mm (H7/g6, h6, p6) | Optical & Probe CMM |
*Where a mating bore, thread, or datum requires tighter accuracy than BS EN 10243-1 or ASTM B247 allows, we forge the blank and finish-machine that feature on in-house CNC cells.
| Dimension (mm) | Up to 50 mm | 50 to 120 mm | 120 to 200 mm | 200 to 300 mm |
|---|---|---|---|---|
| Class F (Fine) | 0.6 mm | 0.8 mm | 1.0 mm | 1.3 mm |
| Class C (Coarse) | 1.2 mm | 1.6 mm | 2.0 mm | 2.6 mm |
| Net Weight (kg) | Up to 0.5 kg | 0.5 to 1.5 kg | 1.5 to 3.0 kg | 3.0 to 6.0 kg |
|---|---|---|---|---|
| Class F (Fine) | +0.6 / −0.3 mm | +0.9 / −0.4 mm | +1.1 / −0.5 mm | +1.4 / −0.7 mm |
| Class C (Coarse) | +0.9 / −0.4 mm | +1.3 / −0.6 mm | +1.6 / −0.8 mm | +2.0 / −1.0 mm |
| Net Weight (kg) | Up to 0.5 kg | 0.5 to 2.0 kg | 2.0 to 5.0 kg | 5.0 to 10.0 kg |
|---|---|---|---|---|
| Plus (+ mm) | +0.80 mm | +1.00 mm | +1.50 mm | +2.00 mm |
| Minus (− mm) | −0.40 mm | −0.50 mm | −0.80 mm | −1.00 mm |
| Length (mm) | Straightness (mm) | Net Weight (kg) | Max Die Mismatch (mm) |
|---|---|---|---|
| 0 to 250 mm | 0.80 mm | Up to 1.0 kg | 0.50 mm |
| 250 to 500 mm | 1.50 mm | 1.0 to 3.0 kg | 0.80 mm |
| 500 to 1000 mm | 2.50 mm | 3.0 to 10.0 kg | 1.00 mm |
| Over 1000 mm | 4.00 mm | 10.0 to 20.0 kg | 1.50 mm |
IATF 16949:2016 Quality, NDT & CMM Inspection
Every hot forging cell runs under IATF 16949:2016 with full heat-lot traceability from billet chemistry through induction heating, die pressing, heat treatment, and final CNC inspection.
| Stage | What We Check | Deliverable |
|---|---|---|
| Incoming Billet (IQC) | Alloy spectro-chemistry, bar diameter, and heat-lot verification | EN 10204 3.1 Certs |
| Hot Press & Heat Treat (IPQC) | Billet temperature (650–1300 °C), die closure, mismatch, and Rockwell/Brinell hardness | SPC & Heat Treat Logs |
| Final Machined (FQC) | CMM dimensional layout, ultrasonic/dye-penetrant NDT, and thread gauges | CMM, FAIR & PPAP |
Certified to IATF 16949:2016 with APQP and PPAP submission on request. For aerospace forgings, we supply EN 10204 3.1 certs, FAIR, CMM, and NDT, and disclose up front that Meco is not AS9100 or ITAR certified.
Standard Metrology & Non-Destructive Testing
- Ultrasonic & Dye Penetrant NDTDetects subsurface inclusions, forging laps, or thermal cracks on safety-critical automotive and heavy machinery forgings.
- Automated CMM Verification (±0.002 mm)Programmable coordinate measuring machines verify post-forging CNC machined bores, datums, and GD&T callouts.
- Post-Quench Hardness & Grain Flow ChecksVerifies mechanical properties after normalising, quenching and tempering, or T6 aluminum aging.
- Turnkey Sub-Assembly & Global FulfillmentFinished hot forgings integrate directly into mechanical sub-assemblies and ship from our Thailand and China plants.
Hot Forging Tooling, Cost & Sourcing Resources
Practical engineering guides on custom forging dies, metal part pricing, and alloy selection.
- FORGING & DIES
- PRICING & ROI
- MATERIALS & CERTS
Swipe sideways to view all resource categories.
Frequently Asked Questions
What tolerances and part weights can your hot forging presses hold?
We produce closed-die hot forgings from 0.1 to 50 kg (0.22 to 110 lbs) and open-die or ring-rolled forgings from 5 to 50 kg (11 to 110 lbs). Steel drop forgings hold BS EN 10243-1 Class F (0.6 mm up to 50 mm nominal; 1.3 mm at 200–300 mm), and aluminum forgings follow ASTM B247. Critical bores, threads, and mating faces are finish-machined in-house on our CNC machining cells to ±0.01 mm (±0.0004″), verified by ±0.002 mm CMMs.
When should I choose hot forging over cold forging or metal casting?
Choose hot forging (650 to 1300 °C / 1200 to 2370 °F) when your component requires high impact toughness, fatigue resistance, and complex 3D geometry—such as steering knuckles, axles, yokes, gear blanks, and high-pressure valve bodies. Unlike metal casting, hot forging eliminates internal gas porosity and aligns grain flow with part contours. Choose cold forging for smaller, symmetrical parts (0.01 to 5 kg) at volumes above 50,000 pieces.
How much does customized hot forging tooling cost, and what is the lead time?
Custom hot forging die build and first-article sampling take 6 to 12 weeks depending on part size and cavity complexity. Because generic online die tables are inaccurate, send us your 3D CAD and 2D drawing for an itemised die and piece-price quote inside 24 hours—including written tooling ownership terms and free DFM feedback that typically cuts part cost by 15% to 30%.
What are your minimum order quantities (MOQ) for hot forged parts?
We have no minimum order quantity (no MOQ)—scaling from 10 prototypes to 10 million+ production parts. Closed-die hot forging is most economical at 1,000+ parts per year. For prototype validation or runs under 200 pieces, we quote open-die forging or billet CNC machining side-by-side and can machine your initial bridge parts in 1 to 2 weeks while your production die is cut.
Do you handle heat treatment, CNC machining, and surface finishing in-house?
Yes. Meco owns and operates 20,000 m² in Thailand and 16,000 m² in China under IATF 16949:2016. Your hot forged blanks go directly to our in-house heat treatment lines (normalising, quenching & tempering, T6 aging), multi-axis CNC machining centers, and 40+ surface finishing lines on one purchase order with signed NDA protection.
How to Get Started
Submit STEP/IGES models, PDF drawings, alloy grade, and annual volume via our NDA-protected quote form.
Receive itemised hot forging die and unit pricing in under 24 hours with DFM tips to save 15–30%.
We cut the hot forging dies and press first-article samples in 6 to 12 weeks (or CNC-machine bridge billets in 1–2 weeks).
Forgings are heat treated, machined to ±0.01 mm (±0.0004″), and verified via CMM, NDT, FAIR, and EN 10204 3.1 certs.
Scale up to 10M+ parts across our Thailand and China plants with surface finishing and sub-assembly.
