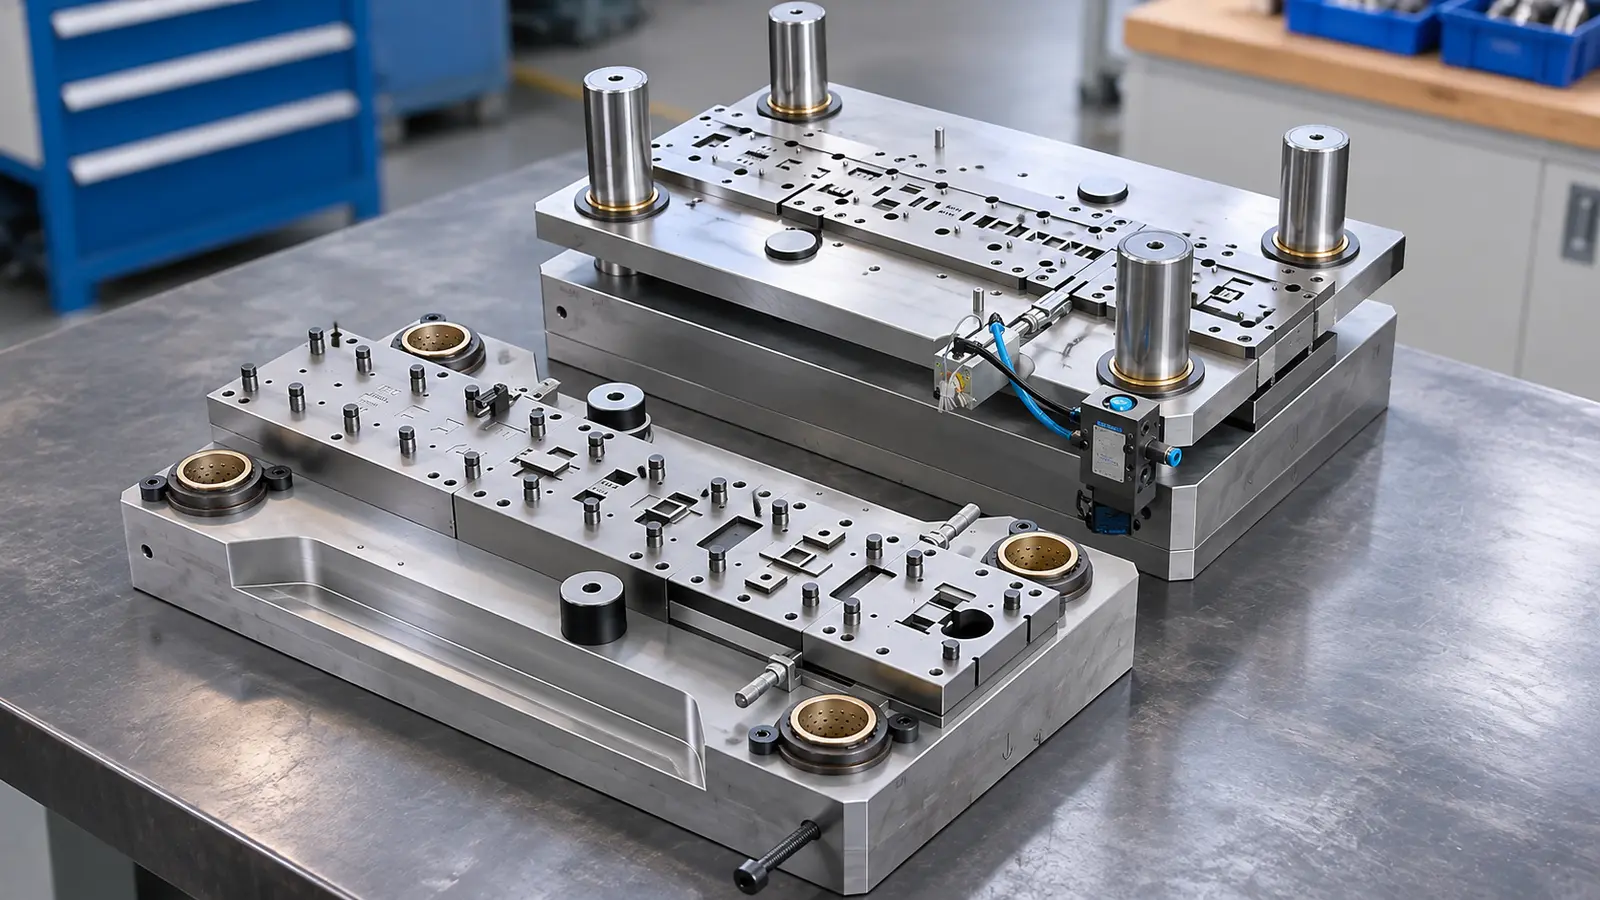
A manufacturing die is a specialized tool used to cut, form, draw or shape material into repeatable parts. Stamping dies shape sheet metal, while casting, forging, extrusion and drawing dies control different processes.
Tool design, workpiece material and production volume determine which die is suitable. Accuracy also depends on the press or machine, process settings, wear and inspection.
Before a stamped bracket, a forged link or a die-cast housing can be produced in quantity, a tool must control its shape. That tool is often called a die. The same word covers several very different manufacturing processes, so choosing the wrong kind can raise tooling cost or make a part difficult to produce. This guide explains what a die does, the main types, how they are made, what they cost and what affects their working life.
Key takeaways
- A die is a tool, not a manufacturing process by itself.
- Cutting dies separate material; forming dies change its shape.
- Progressive, compound and transfer tools differ in how operations and material movement are organized.
- Choose the process by material, geometry, annual quantity and finishing requirements.
- Judge die life and cost using acceptable parts, planned repairs and the inspection plan.
What Is a Die in Manufacturing?
A die is a purpose-built manufacturing tool that controls the shape of material during a defined production operation.
A manufacturing die is a purpose-built tool that controls the shape of a workpiece during cutting, forming, drawing, forging, extrusion or die casting. In a stamping press, a punch and matching die create features in sheet metal. In high-pressure die casting, metal fills a reusable steel die cavity.
The material, tooling arrangement and applied force differ, but the purpose is repeatable part geometry.
For sheet-metal work, compare Meco’s metal stamping capabilities and the die casting service to see how different the tools and materials are.
Dies can punch holes, blank outlines, bend flanges, draw hollow shapes or reproduce cast surfaces. The main benefit is repeatability at a useful production rate. A good die makes parts within specified tolerances over a validated run; it does not make every part literally identical, and it still needs maintenance and inspection.
Die tooling is often economical for medium to high volumes, although simple tools can also be justified for shorter runs.
The word “die” does not refer to one universal machine. A stamping die acts under a press, a drawing die reduces wire or shapes sheet, an extrusion die defines a constant cross-section, and a die-casting die receives injected molten metal. Injection molds also shape plastic, but their process and equipment are not automatically interchangeable with metal dies.
The right tool depends on material, geometry, quantity, tolerance and the expected service life.
Why die selection matters
Two parts can look similar but need different tools. A flat punched bracket, a cast housing with internal ribs and a forged link place different demands on material flow, tooling investment and inspection. The important question is which process meets the drawing at the planned quantity.
The Two Fundamental Categories of Dies in Manufacturing
In sheet-metal manufacturing, dies either separate material or reshape it. Many production tools combine both functions.
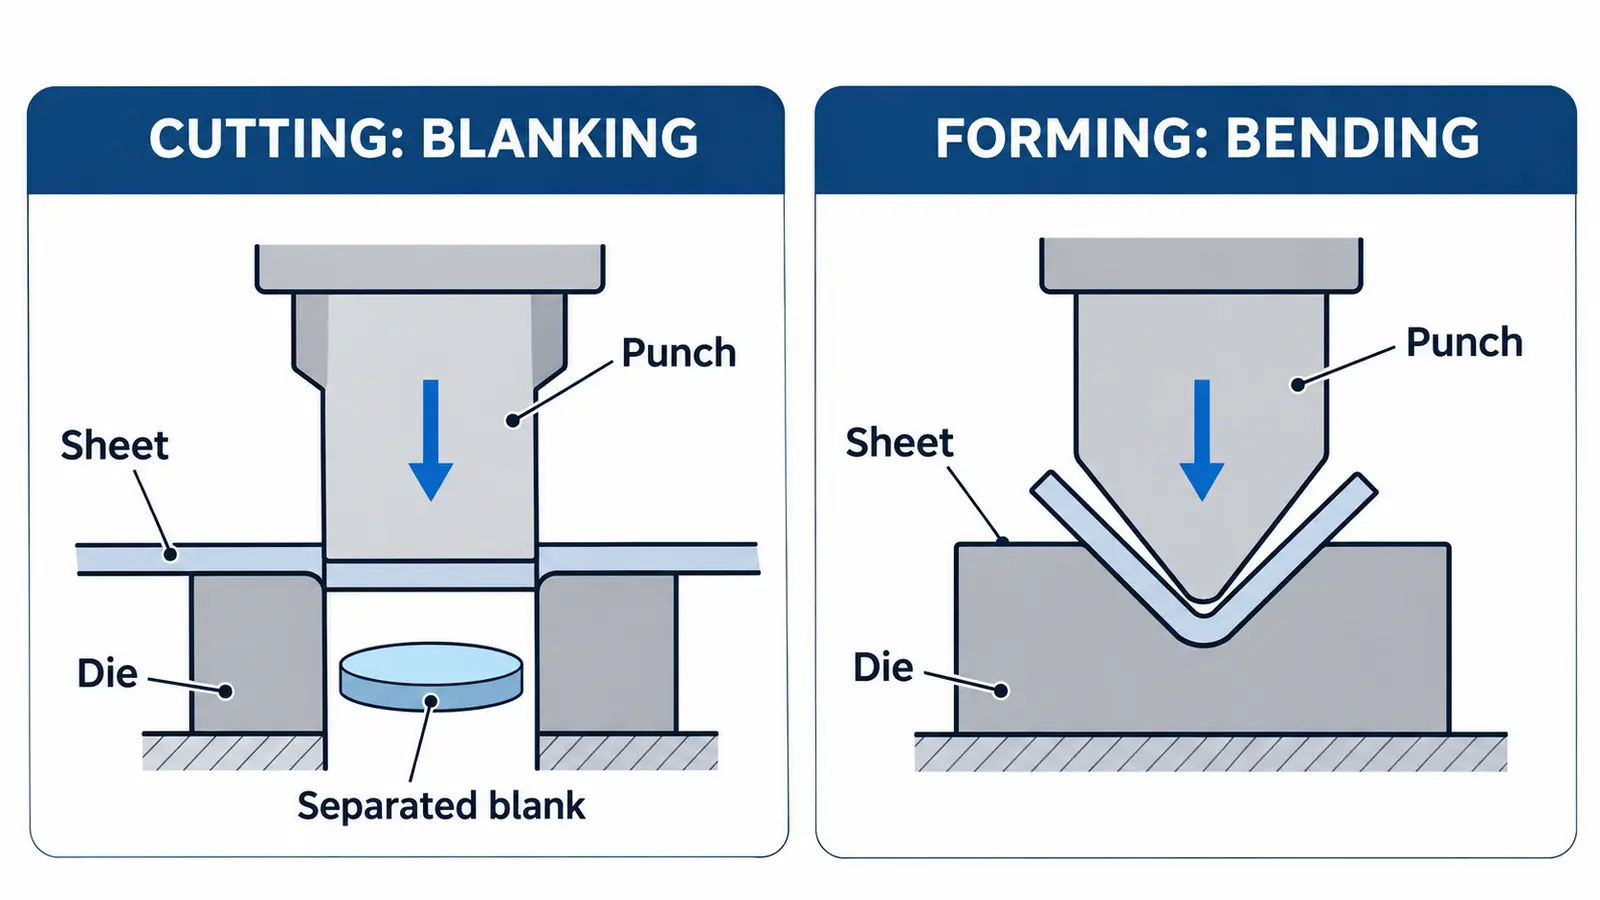
For sheet-metal tooling, the two basic operations are cutting and forming. Cutting dies separate material, as in blanking an outline, piercing a hole or trimming an edge. Forming dies change the sheet’s shape without intentionally cutting it, as in bending, curling, embossing or deep drawing.
A progressive tool can perform both kinds of operation in one coordinated production sequence.
Blanking produces a separated piece that becomes the part, while piercing removes a slug to create a hole in the remaining sheet. Bending pushes the sheet against formed tool surfaces and must account for springback after the force is removed. The distinction is useful when selecting a die design, setting punch-to-die clearance or judging which features need extra support and inspection.
Types of Dies Used in Manufacturing
Die types differ in how they feed material, apply force and produce the required geometry.
The world of dies is broad, spanning processes from cold stamping to high pressure die casting. Each type of die is engineered for a specific manufacturing process and a specific set of material and geometric requirements. What follows is a comprehensive look at the major categories of dies in manufacturing and the roles they serve.
Simple Dies (Single Operation Dies)
A simple or single-operation die performs one operation in one press stroke. A blanking die might cut a bracket outline, while a separate bending die forms one flange. Single-operation tooling is relatively straightforward to build, set up and maintain, though several tools and handling steps may be needed to complete a part.
It can suit low-complexity parts, pilot runs and production quantities that do not justify a more integrated tool.
Compound Dies
A compound die performs two or more cutting operations at the same station during one press stroke. For example, it can pierce a washer’s center hole and blank its outside edge together. Because those features are located by the same tool setup, their relative position can be controlled well.
Compound dies are effective for flat components, but they do not provide the same multi-station sequence as a progressive die.
Progressive Dies
A progressive die uses several stations in a single press tool. A metal strip advances by a controlled feed pitch after each stroke, while the stations work simultaneously on different portions of the strip. The first station may pierce a pilot hole; later stations can blank, emboss, bend or trim features; the part is finally separated at a downstream station.
The material stays attached to the carrier strip until release, so feed accuracy and strip layout are critical.
Meco’s progressive stamping process explains how feeding and stations work together for repeatable high-volume output.
Transfer Dies
Transfer tooling also uses multiple stations, but the workpiece is usually separated from the original strip or blank before it moves between stations. A transfer mechanism lifts or carries that individual workpiece to the next operation. This arrangement works well for deep-drawn shapes, larger components and parts that are difficult to keep on a strip carrier.
Unlike progressive dies, transfer systems must control the orientation and location of each free workpiece.
Casting Dies
A high-pressure die-casting die is a reusable steel mold that defines the cavity for molten nonferrous metal. A machine injects metal into the closed tool; after solidification, the die opens and ejects the casting. Gates, runners, vents, ejector systems and cooling circuits help control how the part forms.
Die-casting dies commonly use heat-resistant tool steels such as H13, but the exact construction depends on the alloy and geometry. Thin walls, ribs and bosses may be cast together, while precise holes or sealing surfaces can still need machining.
For the operating cycle, see the six-step die casting process guide, and compare alloys in the casting material reference.
Forging Dies
Forging dies shape solid metal under compressive force, usually at a temperature chosen for the alloy and the required deformation. In open-die forging, the metal is compressed between relatively simple tools. In impression-die or closed-die forging, shaped cavities guide the material into a more detailed part; flash may still form at the parting line.
The resulting grain flow and soundness depend on billet preparation, tool geometry, temperature and process control, so forging is not an automatic guarantee of superior properties for every application.
For open-die and impression-die routes, review Meco’s custom forging capabilities.
Extrusion Dies
An extrusion die defines the cross-section of material pushed through its opening. Aluminum billets commonly pass through steel extrusion tooling to make long heat sinks, frames and structural profiles. Plastics can also be extruded through purpose-built dies, using a different machine and temperature-control process.
Solid and hollow profiles need different tooling arrangements, including mandrels or bridges for internal voids. Extrusion controls the profile shape along its length, but straightness, twist and final cut dimensions still need verification.
Drawing Dies
The term drawing die covers two different metalworking operations. In wire drawing, a lubricated wire or rod is pulled through a hardened opening to reduce its cross-section. Several dies may be used in sequence for a large total reduction.
In sheet-metal deep drawing, a punch pushes a flat blank into a cavity while a blank holder controls material flow. This is how certain cans, cups, sinks and other hollow shapes are made. The tooling and force paths are different even though both operations are called drawing.
What Are Dies Made Of? Materials That Define Die Performance
Most production dies use specialized tool steels, with carbides or surface treatments for selected wear-intensive features.
Die material affects wear resistance, toughness, heat tolerance, cost and maintenance. Common tool-steel choices include D2 for wear-resistant cutting components, H13 for hot-work applications, and M2 high-speed steel for selected punches or cutting inserts. The best choice depends on the workpiece alloy, tool temperature, edge geometry and expected volume.
A harder die material is not always better if it becomes too brittle under impact.
D2 resists abrasion but needs appropriate edge design and heat treatment to avoid chipping. H13 has good hot-strength and thermal-fatigue resistance, so it is widely used for die casting and hot forging tooling. Cemented carbides can resist wear at high cycle counts, yet their cost and brittleness must be considered.
A buyer should compare projected tool life, repairability, spares and the total cost per accepted part, not just the nominal steel grade.
Heat treatment, grinding, lapping and surface coatings can change how a die performs. Treatments such as titanium nitride (TiN), titanium carbonitride (TiCN) or chromium nitride (CrN) may reduce galling and abrasion for suitable tool-workpiece pairs. No coating can substitute for incorrect clearance, misalignment or weak lubrication.
The resulting life improvement must be established through trials and maintenance records rather than assumed from a generic multiplier.
How Dies Are Made: The Die Manufacturing Process
A production die moves from part requirements and tool design through machining, assembly, tryout and part approval.
Die-making starts by translating the part drawing into a manufacturing sequence. Designers decide which features are blanked, formed, cast or forged and how the workpiece will be located at each step. Computer-aided design (CAD) models help define tool geometry, clearances, feeds and access for maintenance.
Simulations can help expose risks such as uneven metal flow or difficult ejection before steel is cut.
A production tool may also need precision CNC machining and related finishing steps after its initial profile is cut.
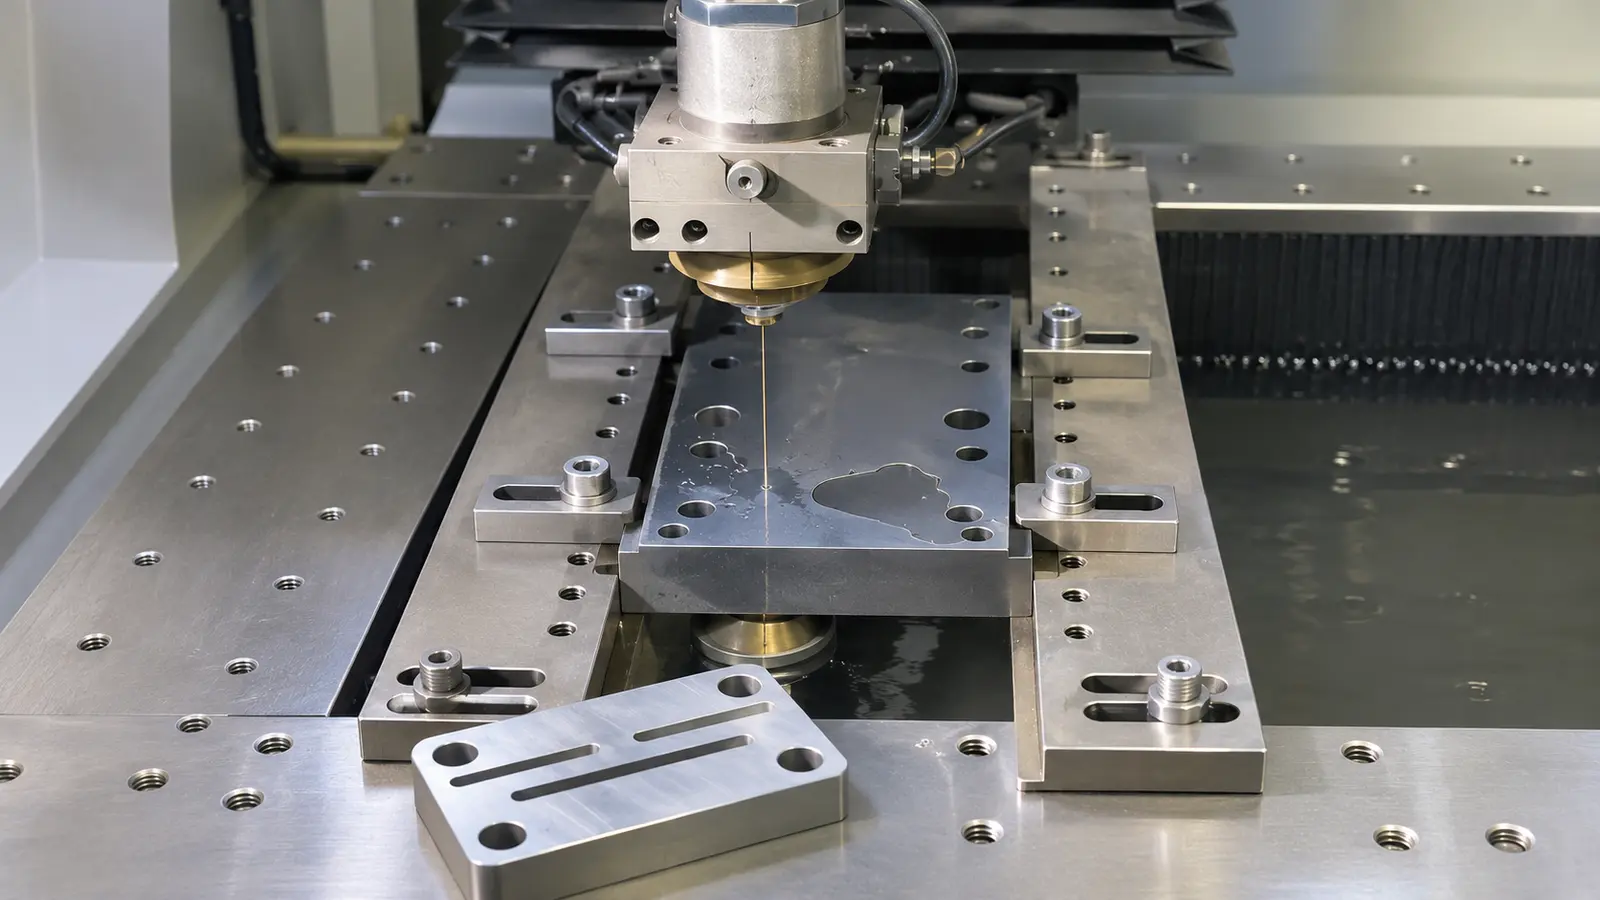
The tool is then made from selected steel and components through milling, grinding, electrical discharge machining (EDM), heat treatment and fitting. Wire EDM can create narrow internal profiles in hardened inserts, while CNC milling removes bulk material and creates larger surfaces. Grinding and fitting bring critical mating components into alignment.
Each operation depends on the die type; not every tool needs every process.
After assembly, the die moves into tryout. Sample parts are checked against the drawing for size, location, surface condition, material flow and visible defects. Toolmakers correct clearances, guide systems, forming details or ejection where the sample shows a problem.
A new tool enters regular production only after its process and acceptance checks are agreed, and any qualification requirements have been met.
Die Life: How Long Does a Manufacturing Die Last?
Tool life varies by process, metal, temperature, loading and maintenance. A quoted life should always state its assumptions.
Die life means the useful period before a tool needs planned repair, significant rework or replacement. There is no single stroke count that applies to stamping, casting and forging alike. Workpiece material, heat cycles, stroke rate, tool steel, lubrication, cleaning, repair strategy and acceptable part tolerances all affect life.
For a quote, request a projected maintenance interval and the assumptions behind it.
For casting programs, the die casting lead-time guide explains where tool build and trial work fit in a larger schedule.
Stamping tools often need periodic punch sharpening, stripper repair and guide-system checks. Die-casting tools can suffer thermal checking and erosion, while forging dies can wear at highly loaded cavity features. Regular part measurements, lubrication checks, coating inspection and spare-insert planning help control downtime.
A life estimate should distinguish strokes or shots, cavities, acceptable parts per cycle and the threshold for refurbishment.
Where Dies Are Used: Industries and Applications
Dies appear in automotive, aerospace, electronics and industrial equipment, but each application calls for different tooling.
Dies are used wherever repeatable shapes are worth the tooling investment. Automotive structures, electrical connectors, industrial enclosures, household appliances and machinery all rely on stamping, casting, forging or extrusion. Different products need different processes because thickness, geometry and service loads are not interchangeable.
Other applications often bring several processes together through whole-product manufacturing.
Automotive Manufacturing
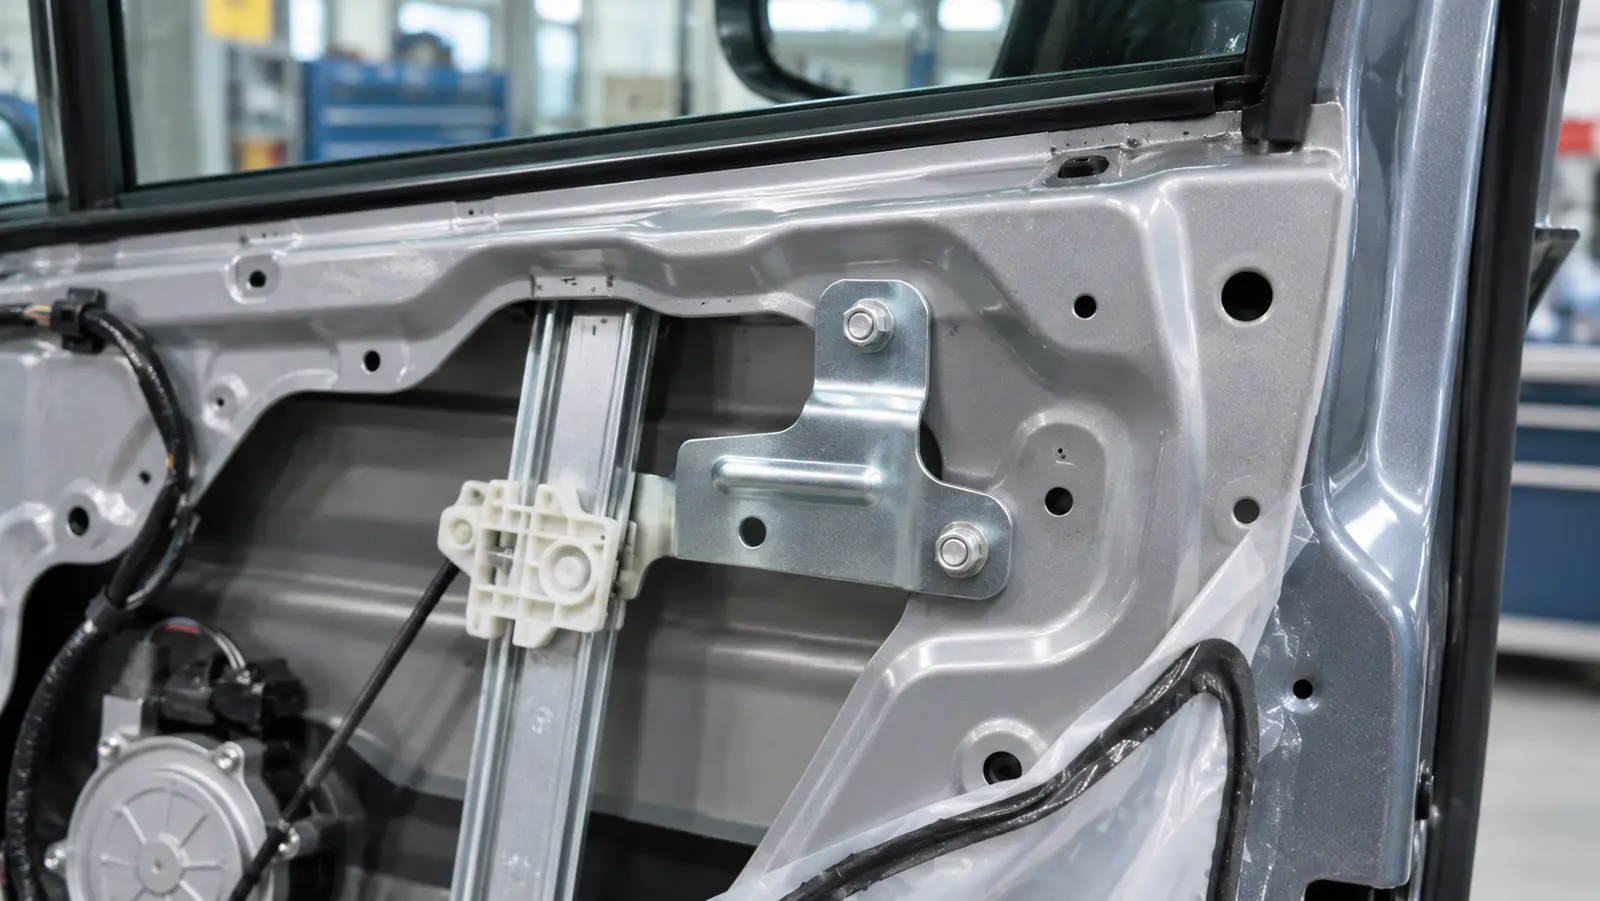
Automotive manufacturing uses several die families in one vehicle. Stamping draws outer body panels and makes brackets, clips and reinforcement details from sheet metal. Die casting can produce selected aluminum or magnesium housings and structural castings, depending on requirements.
Forging shapes highly loaded components such as certain crankshafts and connecting rods. A small door bracket and a large body panel both depend on die control, but they use very different tools and presses.
Aerospace
Aerospace programs use forging, stamping and other forming tools where their material properties and documented processes fit the design. Forged blanks may become structural fittings, disks or landing-gear components after machining and extensive qualification. Sheet-metal dies make brackets, clips and shielding.
Investment casting uses tooling to form wax patterns, not the same high-pressure metal-injection die used for aluminum housings. Every aerospace part still depends on its drawing, process approval and inspection plan.
Consumer Electronics
Consumer electronics use die-cast housings, stamped contacts, shields and small support brackets. Cast metal frames can incorporate bosses and ribs, while progressive dies make thin conductive features in large numbers. Designers must still account for coatings, assembly interfaces and post-process machining when necessary.
Small connector features are especially sensitive to burrs, tool wear and alignment.
Heavy Equipment and Industrial Applications
Heavy equipment uses forged pins and links, stamped covers and guards, cast housings, and extruded profiles. Forging is often considered for loaded components, but the correct process still depends on alloy, heat treatment, required section and fatigue performance. Stamped parts work well when the load can be carried by a thin formed geometry.
Engineers should evaluate finished-part performance rather than choose a process from its name alone.
How Dies Compare Across Manufacturing Processes
Choose the manufacturing process from material, geometry and volume before choosing the die construction.
A die type is usually chosen by the starting material and the shape the finished part needs. Stamping excels with sheet, die casting with complex nonferrous metal shapes, forging with compressed solid-metal blanks, extrusion with constant-section profiles, and drawing with wire or hollow sheet shapes. No one process is best for every quantity or load case.
The die casting process guide gives more detail on molten-metal tooling, while metal stamping focuses on sheet-based components.
Stamping uses a press and shaped sheet-metal tooling to make cut and formed parts, often with fast cycle times. High-pressure die casting injects molten nonferrous metal into a reusable die to make complex near-net-shape parts. Forging forms solid material under compressive load, with machining sometimes required for final features.
Each route has different draft, wall-thickness, tooling-access and material-flow constraints.
Tooling economics depend on more than strokes per minute. An expensive progressive die can become economical when annual volume is high and the strip layout is efficient. Die casting may reduce the number of separate parts in a housing, but needs thermal management, trimming and sometimes machining.
Forging may reduce machining stock or support a required load path, yet its value depends on the drawing and qualification process. Compare total delivered cost and validated capability, not a universal ranking of cycle time or strength.
| Die or process | Starting material | Typical part geometry | Key selection factor |
|---|---|---|---|
| Stamping | Sheet or strip | Thin cut and formed parts | Flat blank layout and annual volume |
| Die casting | Molten nonferrous metal | Ribbed housings and complex walls | Alloy, draft, porosity and tool life |
| Forging | Solid billet or preform | Load-bearing blanks and shaped sections | Load path, grain flow and finishing |
| Extrusion | Billet or polymer melt | Long, constant-cross-section profiles | Profile geometry and post-extrusion control |
| Drawing | Wire, rod or sheet blank | Reduced wire or deep hollow shells | Reduction, lubrication and material flow |
Choosing between die types? Share your drawing, material and target volume for an engineering review of the manufacturing route and tooling tradeoffs.
Talk to an EngineerThe Economics of Dies: What You Need to Know About Cost
The upfront die price is only part of the decision. The useful comparison is total cost per acceptable finished part.
Tooling cost depends on die size, cavity or station count, steel, complexity, expected volume and maintenance. A simple single-operation stamping tool can cost much less than a complex progressive or high-pressure die-casting tool. The important comparison includes setup, material yield, cycle time, secondary work, wear parts, scrap and the number of acceptable pieces delivered.
When the die is only one part of a project, compare it with the wider custom metal-part cost guide and Meco’s tooling and production lead-time guide.
Published prices for simple dies may sit in the low thousands, while large, multi-station or multi-cavity tooling may reach six figures. These are broad industry descriptions, not a Meco quotation or a price rule for a particular design.
For illustration, a $200,000 tool spread across one million accepted parts adds $0.20 per part in tooling amortization; at ten thousand parts, the same tool adds $20 per part before operating costs. Actual quotes need the drawing, alloy, required features, annual demand and production plan.
A more complex die can reduce handling and cost per part at high volumes, but it is not always the best purchase. For a simpler design or shorter run, a single-operation or compound die may offer a lower total delivered cost. Compare tooling payment terms, ownership, repairs, spare components and expected production quantities before choosing the process.
What to confirm before approving a tool
- Part requirements: drawing revision, material, critical dimensions and surface condition.
- Production plan: annual demand, batch size, expected tool life and required spare components.
- Process route: stamping, casting, forging or another method, plus any machining, coating or assembly.
- Validation: first-off samples, measurement method, quality documents and correction process.
- Commercial terms: tooling ownership, maintenance responsibility, transfer arrangements and realistic delivery dates.
Die Tolerances and Quality: What Precision Can You Expect?
Tool precision does not automatically equal finished-part precision. Specify both and validate the production process.
Die-making tolerance and finished-part tolerance are different specifications. The tool must be accurate enough to control the part, but metal springback, thermal movement, wear and process variation change the dimensions after each cycle. A blanket claim such as “all dies hold ±10 microns” is not meaningful without a defined feature, material, measurement method and process.
Ask which dimensions are as-stamped, as-cast or machined afterward.
For casting-specific dimensions, use the die casting tolerance guide, rather than copying one tolerance across every process.
Toolmakers use CNC milling, electrical discharge machining (EDM), grinding and hand fitting to create and maintain precise surfaces. Production validation then measures representative parts against the drawing with suitable gauges and coordinate measuring machines where required. The inspection plan should identify critical-to-function dimensions, expected tool wear, sampling frequency and the process for corrections.
Tightening every dimension unnecessarily can make a die more expensive without improving product function.
Common Die Wear and Failure Modes
Tool wear changes part quality before a die becomes visibly unusable, so regular checks are part of production control.
Dies wear as they cut, form, heat and contact the workpiece. Abrasive wear gradually removes material from high-contact surfaces, while adhesive wear or galling occurs when metal transfers and sticks at the tool interface. Edge damage can increase burr height or shift part dimensions even before a failure is obvious.
Proper lubrication and the correct punch-to-die clearance reduce some of these risks.
Process limits and post-machining requirements can be checked against Meco’s CNC machining services.
Other problems include chipped cutting edges, fatigue cracks from repeated loading and thermal checking in hot-work dies. Those conditions may appear as flash, burrs, rough surfaces or drifting dimensions in the produced parts. Statistical process control, scheduled inspections and planned insert replacement help spot changes early.
The maintenance plan should connect each observed part defect to a plausible tool or machine cause instead of treating every failure as ordinary wear.
What Is a Die in Manufacturing: Why It Matters for Your Next Project
A useful die decision aligns part requirements, tooling investment, production rate and inspection before work begins.
Every manufacturing die solves a repeatability problem: it holds the geometry needed to cut, shape or form material at a practical production rate. A simple blanking die, progressive stamping tool, casting die and forging die all pursue that goal, but they act on different materials and use different equipment. There is no universal die that can replace every other manufacturing process.
A drawing and volume forecast are the starting point for comparing forging, die casting and metal stamping.
For engineers and purchasing teams, the next decision is to match the intended part with a realistic process. Review material, wall thickness, tolerances, annual quantity, available machining allowances, expected tool life and the checks needed for first-off samples. A manufacturing partner can compare tooling scenarios before metal is cut, then plan the transition from approved samples into steady production.
Plan Your Die-Made Part
Meco can review the part drawing, material, expected quantity and downstream operations before recommending a suitable manufacturing route.
- Process review. Stamping, casting, forging and machining options.
- Tooling plan. Geometry, life, maintenance and ownership questions.
- DFM feedback. Comments alongside the quote.
- Quality planning. FAI, PPAP and CMM documentation where specified.
Explore metal stamping, die casting and forging services.
Talk to an Engineer