Custom Investment Casting & Post-Cast CNC Machining Services
Pour small, complex metal parts in stainless steel, carbon and alloy steel, brass, bronze, and titanium into ceramic shell moulds. Get near-net-shape ICI accuracy with in-house CNC machining, heat treatment, and finishing under one roof.
- Stainless 316, 17-4PH & 420, carbon/alloy steel, brass, bronze & titanium
- Wax tooling from $3,000 to $15,000 USD with no minimum order quantity (500–50,000/yr)
- Near-net ICI linear tolerances plus 0.01 mm CNC features (0.002 mm CMM)

- $3,000 – $15,000Low-cost wax pattern tooling
- 0.01 mm CNCMachined features (0.002 mm CMM)
- IATF 16949:2016X-ray, ultrasonic & dye NDT
- Under 24 HoursCosted quote & DFM review
Pre-Tooling DFM & Competitive-Price Investment Casting Machining
Because the wax pattern melts out of a one-piece ceramic shell, undercuts, thin walls, and cored internal passages cast directly with no parting line and minimal machining stock — while pre-tooling DFM removes 15% to 30% of part cost.
- Sealing faces, bores, and threads cut in house to 0.01 mm and ISO 2768 on our custom CNC machining cells
- Integrated metal heat treatment (including 17-4PH aging), shot blasting, powder coat, painting, and surface finishing
- Single purchase order and full lot traceability from raw melt to finished hardware or box-build assembly
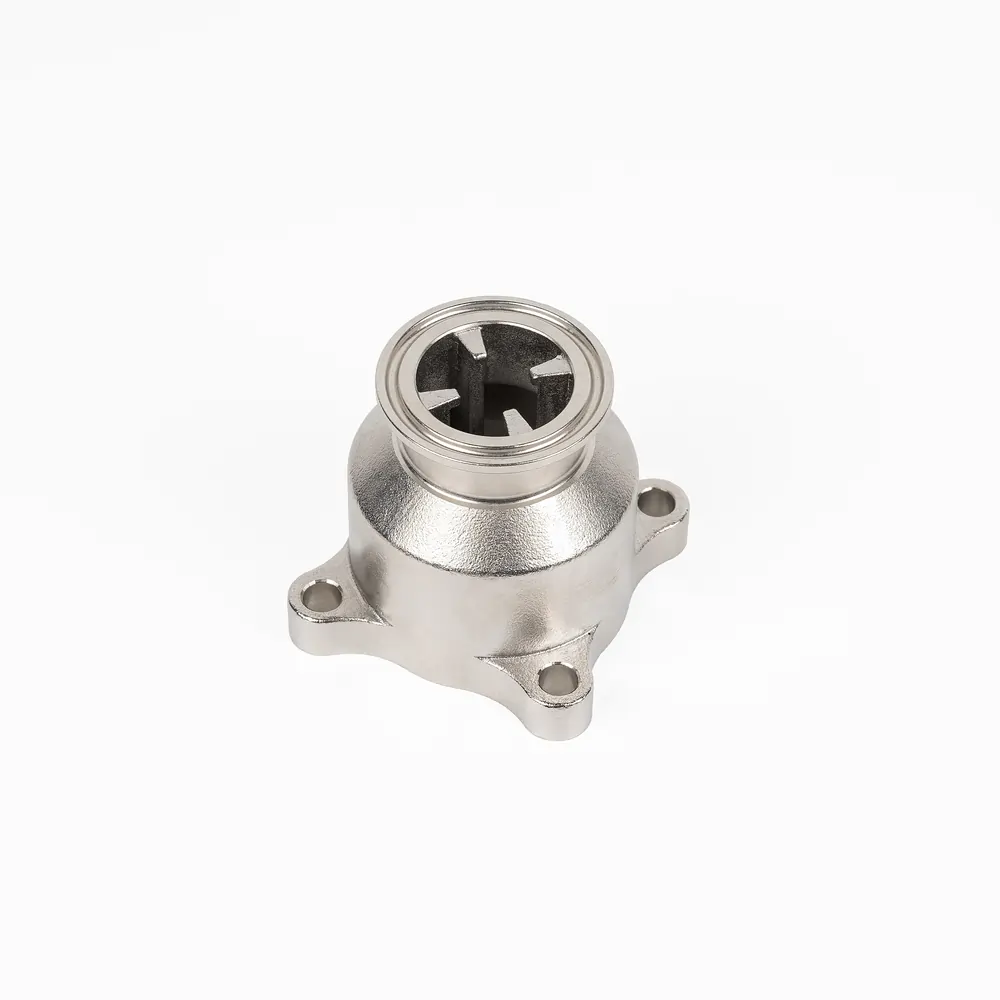
Investment Casting Alloys & Turnkey Post-Processing
Ceramic shells withstand high pour temperatures that ruin permanent dies. Every grade ships with EN 10204 3.1 material certificates. Switch tabs below to review alloys or post-cast operations.
| Material Family | Grades | Why It Is Used & Typical Cast Parts |
|---|---|---|
| Stainless Steel | 316, 17-4PH, 420 | Corrosion resistance and high heat-treated strength (17-4PH); wastewater valve bodies, pump housings, custom hardware fittings, medical instruments |
| Carbon & Alloy Steel | Carbon and alloy steel | High tensile strength, wear resistance, and impact toughness; engine components, drivetrain linkages, levers, latches, heavy equipment wear parts |
| Brass & Bronze | Brass, bronze | Superior castability, bearing properties, and marine/fluid corrosion defense; pump impellers, marine fittings, bushings, architectural hardware |
| Titanium | Titanium | High strength-to-weight ratio and extreme corrosion resistance; aerospace structural fittings and chemical process hardware |
| Process Step | In-House Capability | Customer Benefit |
|---|---|---|
| Post-Cast CNC Machining | Milling, turning, boring, and threading to 0.01 mm and ISO 2768 | Precision sealing faces and bearing bores without managing a second machine shop |
| Heat Treatment | Solution annealing, precipitation hardening (17-4PH), normalizing to drawing spec | Achieves target hardness and mechanical properties prior to final machining |
| Surface Finishing | Shot blasting, polishing, powder coating, and industrial painting | Clean, cosmetic, or corrosion-resistant surfaces per our surface finish chart |
| NDT & Metrology | CMM to 0.002 mm plus X-ray, ultrasonic, and dye penetrant NDT | Verifies internal soundness and tight GD&T before shipment |
Investment Casting vs. Sand, Die Casting & MIM
Compare where lost-wax investment casting beats sand casting, high-pressure die casting, and metal injection molding (MIM) on detail, alloy range, and tooling spend.
| Feature | Investment Casting | Sand Casting | High-Pressure Die Casting | Metal Injection Molding |
|---|---|---|---|---|
| Typical Tolerance | Near net shape per ICI | ISO 8062 CT9 to CT10 | NADCA standard 0.010 in | Near net shape |
| Tooling Cost | Wax tool $3,000–$15,000 Low Tool $ | Patterns $500 to $5,000 | Dies $20,000 to $150,000+ | Tooling 6 to 10 weeks |
| Ideal Volume | 500 to 50,000 / year (No MOQ) | 50 to 5,000 / year | 5,000 to 1,000,000+ | 5,000 to 500,000+ |
| Lead Time | 6 to 12 weeks | 4 to 8 weeks | 6 to 14 weeks | 6 to 10 weeks (tooling) |
| Metals Available | Steel, SS, brass, bronze, Ti | Al, steel, SS, brass, bronze | Aluminum, zinc, magnesium | Sintered metal powders |
| Part Size & Stock | Small & intricate | Low stock | Up to 100 kg | Highest stock | Small to medium | Low stock | Very small | Low stock |
| Best Application | Valve bodies, impellers, fittings | Large, low volume, prototypes | Thin-wall housings at volume | Small complex parts at volume |
*For one-off prototypes under 100 pieces, CNC machining from bar or billet requires zero tooling. See our 2026 metal part pricing guide for full cost breakdowns.
Need Small, Complex Metal Parts Cast & Machined Under One Roof?
Send us your STEP/IGES files and annual volume. Receive a wax tooling and piece-part quote with DFM notes in 24 hours.
ICI Casting Tolerances, Standards & DFM Guidelines
Review our as-cast ICI linear standards and post-cast 0.01 mm CNC machining tolerances alongside our ceramic-shell DFM rules.
| Parameter | Meco Specification | Notes & Applied Standards |
|---|---|---|
| As-Cast Tolerance | Near net shape per ICI | ICI linear tolerance & GB/T 6414 general specifications agreed at DFM |
| Dimensional Standards | ISO 8062-3, ISO 286, ANSI B4.1 | Tighter than ISO 8062 CT9–CT10 sand casting tolerances |
| Machined Features | 0.01 mm & ISO 2768 | Sealing faces, bores, and threads cut on in-house CNC machining cells |
| CMM & NDT Inspection | CMM to 0.002 mm | Supported by X-ray, ultrasonic, and dye penetrant non-destructive testing |
*Attach a 2D PDF drawing to nominate critical bores, threads, and mating faces for 0.01 mm post-cast CNC machining.
| Design Rule | Engineering Recommendation | Cost & Quality Impact |
|---|---|---|
| Wall Section Uniformity | Keep wall thickness consistent across the part | Ensures the ceramic shell fills and cools evenly without shrinkage |
| Internal Corners | Use smooth radii rather than sharp internal corners | Prevents shell cracking and stress concentrations during solidification |
| Heavy Sections | Avoid isolated heavy sections that require extra feeding | Reduces gating complexity, shell build time, and unit casting cost |
| Mating Faces & Bores | Add machining stock to every critical sealing face and bore | Allows in-house CNC cells to finish features to 0.01 mm and ISO 2768 |
IATF 16949:2016 Quality, NDT & Lot Traceability
Every investment casting cell operates under IATF 16949:2016 (incorporating ISO 9001:2015), delivering full lot and serial traceability from melt to final shipment.
| Inspection Stage | Verification Method | Deliverables |
|---|---|---|
| Alloy & Melt (IQC) | Chemical composition verification per heat lot | EN 10204 3.1 & CoA |
| Internal Integrity (NDT) | X-ray radiography, ultrasonic testing & dye penetrant | NDT Inspection Reports |
| Dimensional Metrology | CMM verification resolving to 0.002 mm on machined features | FAIR & PPAP Submissions |
Complete PPAP, First Article Inspection (FAI), Certificate of Analysis (CoA), and EN 10204 3.1 documentation supplied on request.
Industries & Applications We Cast For
- Industrial Valves, Pumps & Wastewater EquipmentOne-piece cored stainless 316 and bronze valve bodies, pump housings, and impellers with CNC-machined sealing faces.
- Automotive Engine & Heavy EquipmentHeat-resistant stainless exhaust/drivetrain engine components, alloy steel wear parts, lever arms, linkages, and couplings.
- Aerospace & Medical Equipment17-4PH, 316 stainless, and titanium structural fittings, latches, levers, and cleanable surgical instrument bodies.
- Telecom, Electronics & Commercial HardwareCoastal-grade stainless telecom pole clamps, washdown electronics housings, furniture brackets, and lighting fittings.
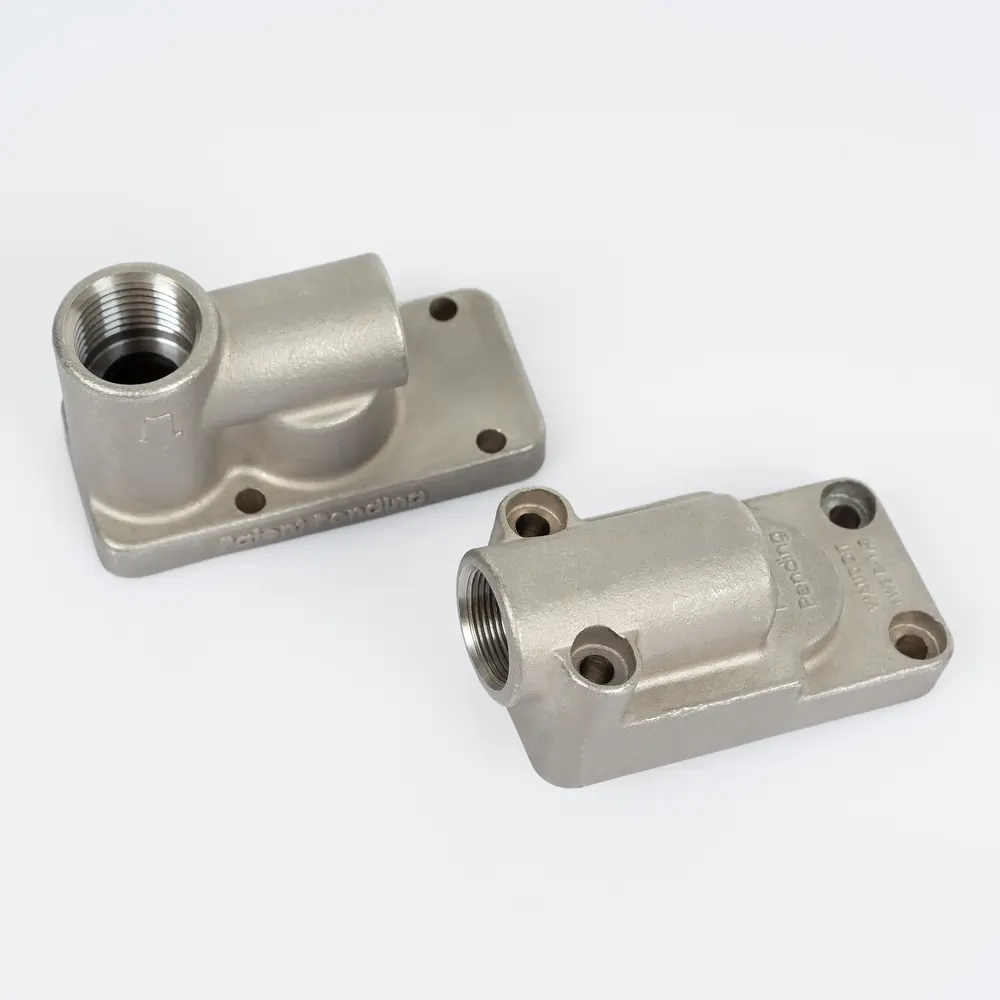
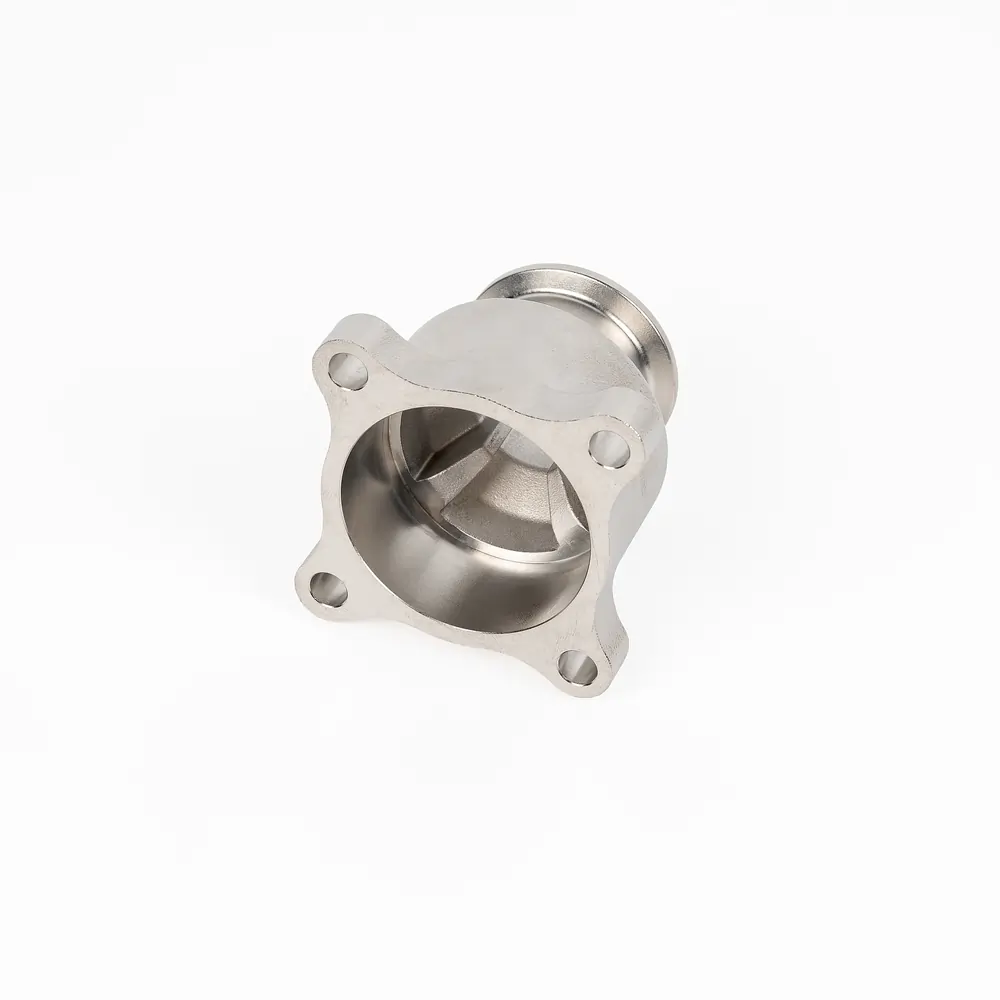
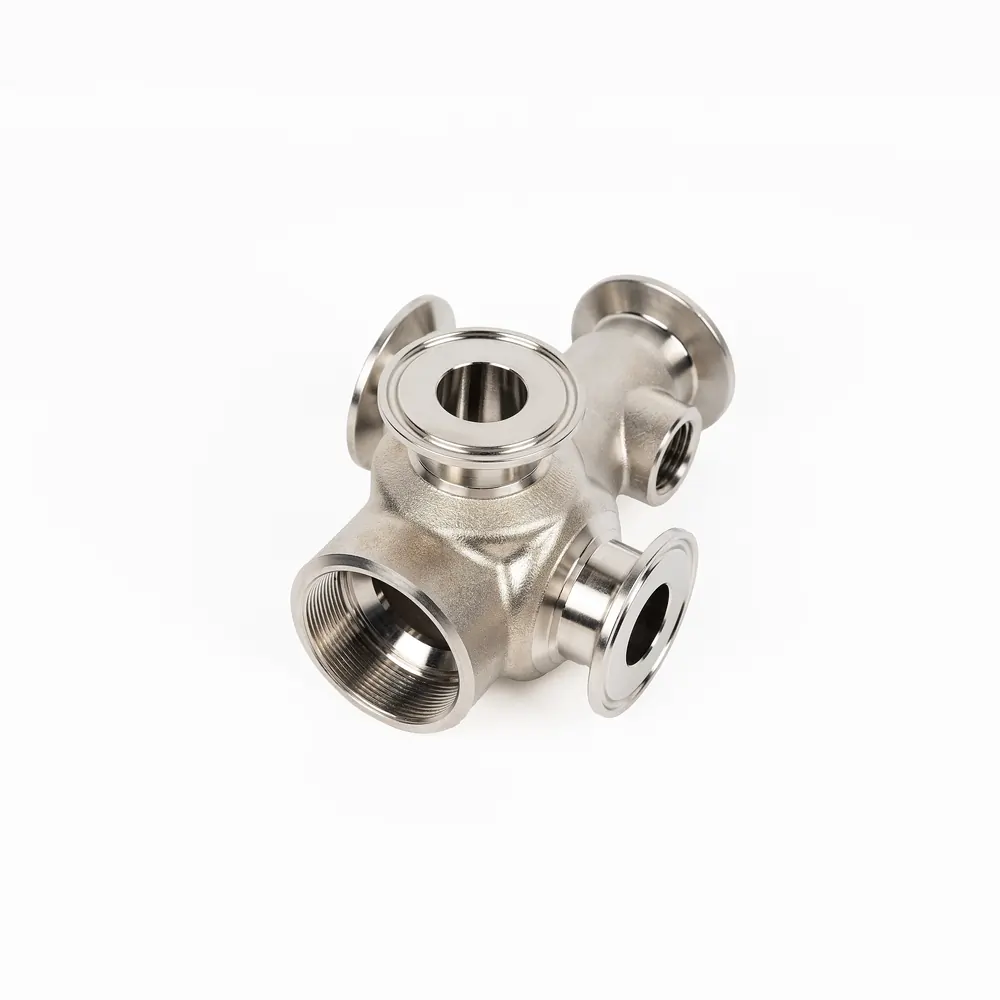
Swipe to view recent investment cast parts.
Frequently Asked Questions
How much does investment casting wax tooling cost, and what drives part price?
Wax tooling runs $3,000 to $15,000 USD — well below a permanent gravity or die casting die. Unit price depends on pattern complexity, shell build time, alloy grade, part weight, annual volume, and required CNC machining or finishing. Free DFM changes agreed before cutting the wax tool typically remove 15% to 30% of part cost.
What alloys can Meco pour via custom investment casting?
We pour stainless steel (316, 17-4PH, and 420), carbon and alloy steel, brass, bronze, and titanium. Because the ceramic shell is disposable, it handles high-melting-point, wear- and corrosion-resistant alloys that would destroy a permanent die casting mould. Every lot ships with EN 10204 3.1 material certificates on request.
What tolerances can your investment casting and CNC machining cells hold?
Castings arrive near net shape to ICI linear tolerance (alongside GB/T 6414, ISO 8062-3, ISO 286, and ANSI B4.1 standards), which is significantly tighter than ISO 8062 CT9–CT10 sand casting. For critical sealing faces, bores, and threads, we machine features in house to 0.01 mm and ISO 2768, verified on a CMM resolving to 0.002 mm.
How do I choose between investment casting, sand casting, die casting, and MIM?
Investment casting wins on small, intricate parts in hard alloys (stainless, steel, titanium) at 500 to 50,000 parts a year because it leaves minimal machining stock. Sand casting wins on large parts up to 100 kg or runs under 500 pieces ($500–$5,000 patterns). Die casting wins above 5,000 parts a year but is limited to aluminum, zinc, and magnesium. For very small complex parts at high volume, consider metal injection molding (MIM).
What is your minimum order quantity (MOQ) and production lead time?
We have no minimum order quantity (no MOQ) — supporting single-piece prototypes through economical runs of 500 to 50,000 parts per year. Quotes with DFM feedback return inside 24 hours, and production lead time is 6 to 12 weeks from approved wax tooling and released PO.
How to Get Started
Send your STEP or IGES file with alloy, annual volume, tolerances, and finish. Response in under 24 hours.
Receive itemized wax tooling and piece pricing plus DFM notes on wall sections, radii, and machining stock to cut cost by 15–30%.
We build the wax tool ($3,000–$15,000), pour the ceramic shell, and deliver first articles with CMM and NDT reports.
After PPAP approval, we run casting, 0.01 mm CNC machining, heat treatment, and finishing, shipping from North America or Asia.
