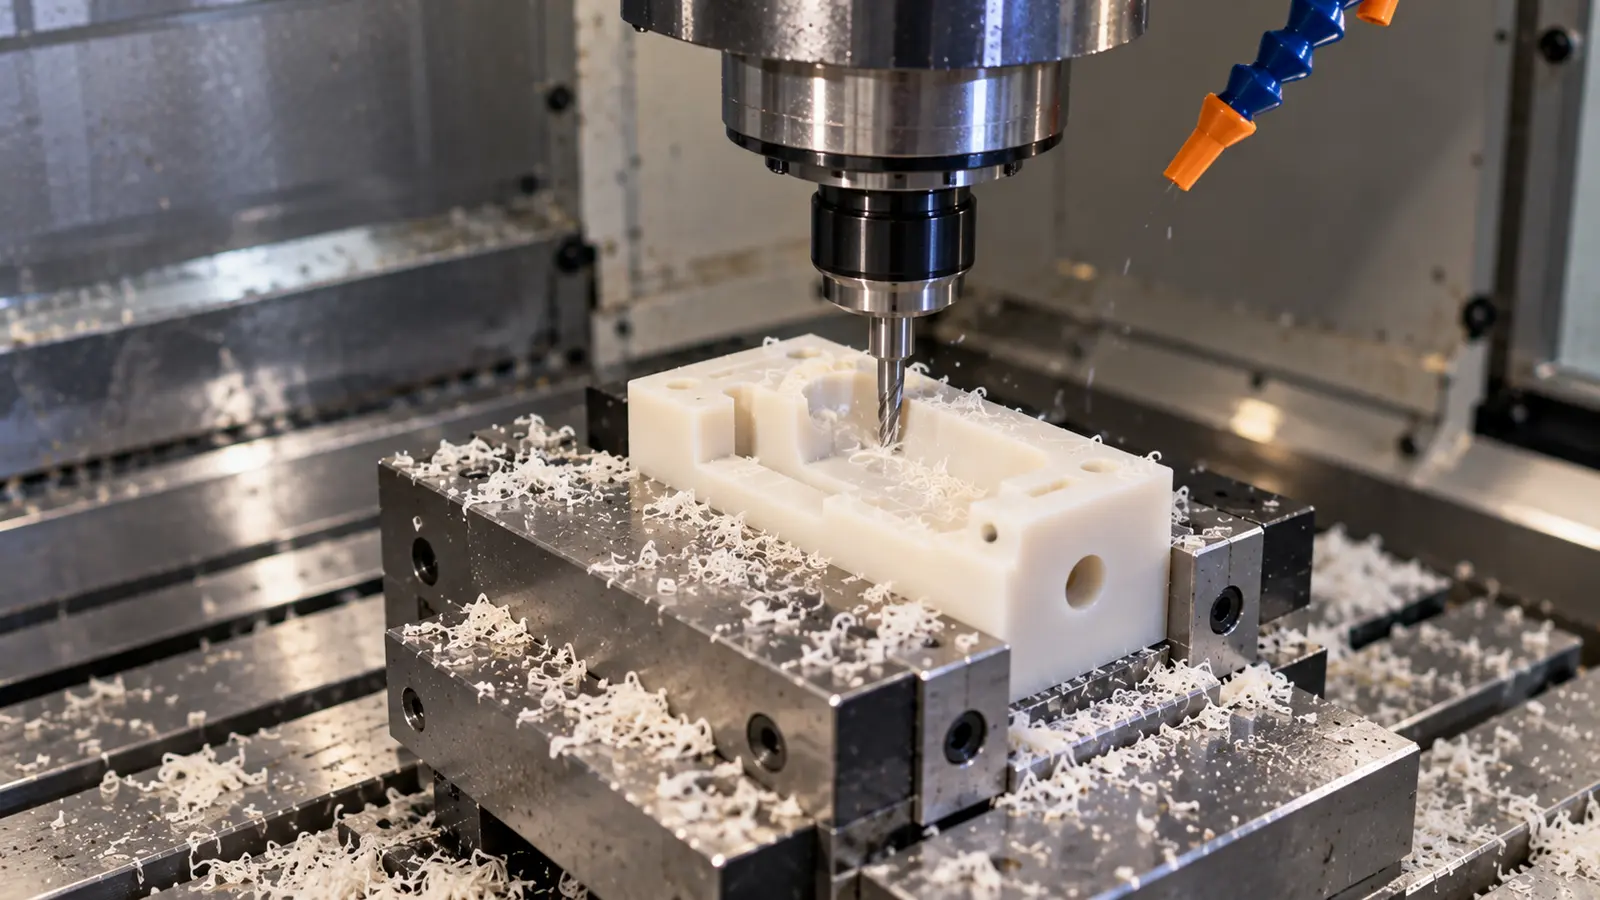
Medical plastics machining uses CNC processes to produce precise polymer components from materials such as PEEK, UHMWPE, POM, PTFE, PEI and nylon.
Material grade, heat control, workholding, biocompatibility evidence and lot traceability all need to be considered together, especially for patient-contact applications.
Engineering polymers have reshaped how the medical industrial sector designs everything from spinal fusion cages to single-use diagnostic housings. Where titanium and stainless steel once dominated, plastics such as PEEK, UHMWPE and POM now deliver comparable mechanical performance at a fraction of the weight, with radiolucency that simplifies post-operative imaging.
Yet realizing those benefits demands a machining partner that understands polymer-specific tool paths, biocompatibility documentation and the traceability rigor that medical OEMs expect.
This guide examines the materials, CNC processes and regulatory frameworks that underpin successful medical plastics machining, and explains how medical precision manufacturing disciplines translate from metals to high-performance polymers.
It is the fourth article in a four-part series on medical manufacturing. For a broader overview of CNC processes, metal materials and partner selection, see the pillar guide on medical CNC machining.
Key Takeaways
- Six engineering plastics dominate medical applications: PEEK, UHMWPE, POM (Delrin), PTFE, Ultem (PEI) and Nylon (PA), each with distinct biocompatibility profiles and machining behaviors.
- CNC machining of medical plastics routinely holds tolerances of +/-0.025 mm and surface finishes down to Ra 0.4 micrometers, meeting both implant-grade and instrument-grade requirements.
- Biocompatibility testing follows FDA guidance on ISO 10993-1 and the current ISO 10993-1:2025 framework; material selection must align with device contact type and duration.
- CNC machining complements plastic injection molding by handling low-to-mid volumes, tight tolerances and design iterations without tooling investment.
- Quality is validated through IATF 16949 processes including PPAP, FAI, CMM inspection, full lot traceability and material Certificates of Analysis (CoA).
Why Engineering Plastics Are Gaining Ground in the Medical Industrial Sector
The global medical device market reached USD 678.88 billion in 2025 and is projected to grow to USD 719.61 billion in 2026, with North America accounting for more than 40 percent of that total. Inside this expansion, polymer-based components are among the fastest-growing segments because they address challenges that metals cannot easily solve.
- Weight reduction is the most visible advantage. A PEEK spinal interbody cage weighs roughly 60 percent less than a comparable titanium cage, easing patient comfort and reducing shipping costs for single-use kits.
- Radiolucency is equally important: unlike metallic implants, PEEK and UHMWPE do not produce scatter artifacts on CT or MRI scans, giving surgeons a clearer view of healing tissue.
- Chemical resistance allows polymers such as PTFE and POM to survive repeated autoclave sterilization at 134 degrees Celsius without dimensional drift, a property that extends the service life of reusable surgical instruments.
- Finally, electrical insulation makes plastics the default choice for housings and connectors in powered diagnostic equipment, where patient-leakage-current limits are measured in microamps.
These properties explain why medical equipment manufacturers increasingly specify plastics for Class I and Class II devices and, in select FDA-cleared applications, for Class III implantable components.
Medical-Grade Plastics: Properties, Standards and Typical Applications
Not all plastics are equal in regulated environments. The table below compares the six polymers most frequently specified in medical plastics machining programs, together with the biocompatibility standards each typically satisfies.
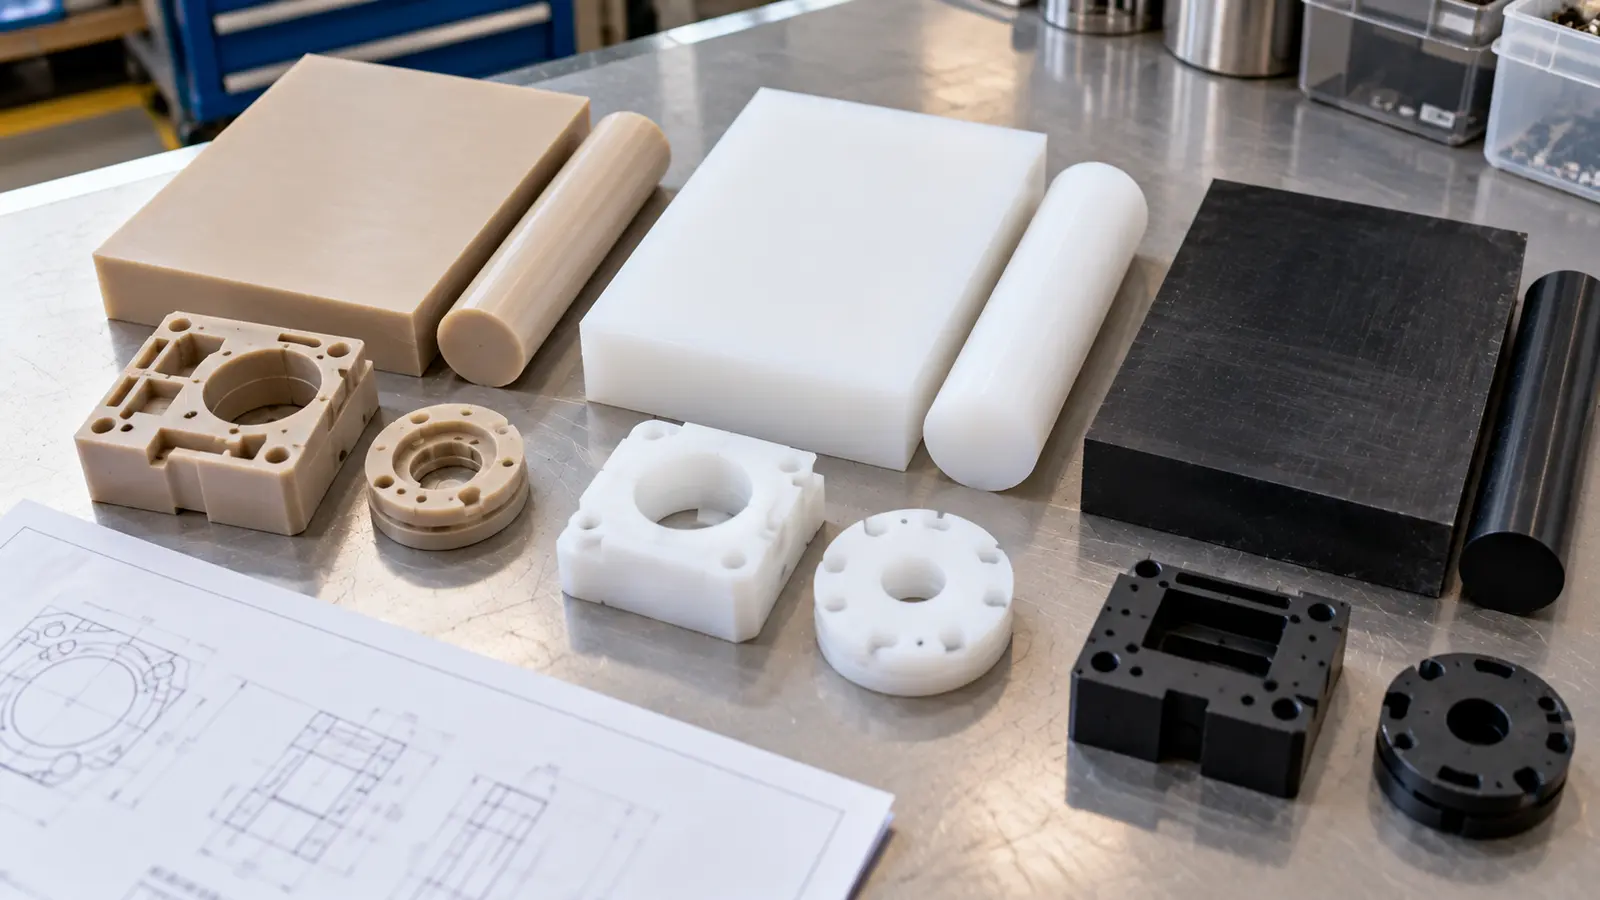
| Material | Key Properties | Biocompatibility Standard | Common Medical Applications |
|---|---|---|---|
| PEEK (Polyetheretherketone) | Tensile strength ~100 MPa; continuous use to 250 C; radiolucent; autoclavable | ISO 10993-1:2025, USP Class VI, ASTM F2026 | Spinal fusion cages, dental abutments, arthroscopic guides, trauma fixation plates |
| UHMWPE (Ultra-High-Molecular-Weight Polyethylene) | Exceptional wear resistance; low coefficient of friction; self-lubricating; gamma-sterilizable | ISO 10993, USP Class VI, ASTM F648 | Acetabular liners (hip), tibial inserts (knee), glenoid components (shoulder) |
| POM / Delrin (Polyoxymethylene) | High stiffness; low moisture absorption; excellent dimensional stability | FDA 21 CFR, USP Class VI (select grades) | Inhaler bodies, insulin pen mechanisms, luer connectors, valve components |
| PTFE (Polytetrafluoroethylene) | Lowest coefficient of friction of any solid; chemical inertness; service range -200 to +260 C | ISO 10993, USP Class VI, FDA 21 CFR 177.1550 | Catheter linings, seals and gaskets, fluid-path bushings, non-stick coatings on instruments |
| Ultem / PEI (Polyetherimide) | High strength-to-weight; inherent flame resistance; transparent amber color for visual inspection | ISO 10993, USP Class VI (medical grades) | Sterilization trays, surgical light handles, reusable instrument housings, fluid reservoirs |
| Nylon / PA (Polyamide 6, 6/6, 12) | Good fatigue resistance; moderate temperature range; low cost | FDA 21 CFR (food and limited body contact) | Cable ties in device assemblies, non-contact housings, guide bushings, gear-driven actuators |
Material Selection Tip
For any component that contacts tissue or bodily fluids for more than 24 hours, the FDA expects biocompatibility evaluation aligned with the current ISO 10993-1:2025 framework. Start with a biological evaluation plan that maps the device's contact type, contact duration and body location before choosing a polymer grade.
CNC Processes Used in Medical Precision Manufacturing of Plastics
Machining medical-grade plastics shares many principles with metal cutting but introduces unique variables: lower thermal conductivity causes localized heat build-up, hygroscopic resins such as Nylon can swell from absorbed moisture, and softer polymers may deflect under standard clamping forces. The processes below address these challenges while meeting the tolerance bands medical OEMs require.
3-Axis and 5-Axis CNC Milling
Three-axis milling covers the majority of prismatic plastic components, including rectangular housings, flat surgical guides and manifold blocks. When the geometry demands undercuts, compound angles or thin-wall pockets, 5-axis CNC machining eliminates secondary setups and the re-fixturing error that accompanies them.
For a PEEK arthroscopic guide, for example, a single 5-axis operation can machine the curved bone-contact surface, through-holes for K-wires and a flat mounting boss in one clamping, holding true position within 0.05 mm across all features.
CNC Turning
CNC turning produces cylindrical plastic parts such as luer bodies, syringe barrels, PTFE valve seats and POM threaded connectors. Swiss-type lathes are particularly effective for small-diameter medical plastics (under 25 mm) because the guide bushing supports the workpiece close to the tool, limiting deflection in a material that is inherently less rigid than steel.
CNC Drilling and Tapping
CNC drilling and tapping in plastics require peck cycles and controlled feed rates to evacuate chips without melting the bore wall. Thread-forming taps are often preferred over cutting taps for thermoplastics because the displaced material creates a denser, stronger thread flank without generating chips that could become particulate contaminants.
Micro-Machining
Endoscopic components, micro-fluidic channels and hearing-aid housings feature geometries below 0.5 mm. Micro-milling with spindle speeds above 40,000 RPM and diamond-coated end mills produces these features in PEEK and PEI while maintaining tolerances of +/-0.010 mm and surface finishes below Ra 0.8 micrometers.
Tolerances and Surface Finish for Machined Medical Plastics
Polymer parts generally require wider tolerances than metals of the same geometry because plastics have higher coefficients of thermal expansion and lower elastic moduli. However, with controlled environment machining (stable ambient temperature of 20 +/-2 C), stress-relieved stock and the right fixturing strategy, medical plastic parts can achieve tolerances that rival many metal applications.
| Parameter | Standard Grade | Precision Grade | Notes |
|---|---|---|---|
| Linear tolerance | +/-0.05 mm | +/-0.025 mm | Precision grade requires stress-relieved bar stock and temperature-controlled environment |
| Geometric tolerance (true position) | 0.08 mm | 0.04 mm | Best achieved with 5-axis single-setup strategy |
| Surface finish (Ra) | 1.6 micrometers | 0.4 micrometers | Fluid-contact surfaces may require Ra less than 0.8 micrometers to limit bacterial adhesion |
| Minimum wall thickness | 1.5 mm | 1.0 mm | Below 1.0 mm only with custom fixturing and low-vibration tool paths |
| Hole diameter tolerance | +/-0.05 mm | +/-0.02 mm | Reaming after drilling is recommended for precision bores in PEEK and POM |
Surface finish is not merely cosmetic in medical devices. Rougher surfaces create micro-cavities where bacteria can colonize, while overly polished bearing surfaces in joint implants can increase adhesive wear. The target Ra must therefore be specified per functional zone, a practice that begins during DFM review.
Biocompatibility: Standards, Testing and Material Traceability
Biocompatibility is the property of a material to perform with an appropriate host response when applied as intended. For machined plastic components that will contact a patient, the regulatory framework rests on two pillars: the ISO 10993-1:2025 standard (sixth edition, replacing the now-withdrawn 2018 version) and, in the United States, the FDA guidance document on ISO 10993-1 .
ISO 10993 Evaluation Framework
ISO 10993-1:2025 requires a biological evaluation plan that categorizes the device by body-contact nature (surface, externally communicating, or implant) and contact duration (limited, prolonged, or permanent). This sixth edition has been reorganized to align more closely with the ISO 14971 risk management process and introduces updated guidance on exposure duration classification, chemical characterization, and reduction of animal testing.
The contact-type and duration matrix determines which tests apply, including cytotoxicity (ISO 10993-5), sensitization (ISO 10993-10), irritation (ISO 10993-23) and, for implantable devices, systemic toxicity and genotoxicity.
Material suppliers of medical-grade PEEK and UHMWPE typically hold existing test reports for these endpoints, but the device manufacturer remains responsible for evaluating whether the machining process, such as coolant residues or tooling lubricants, could alter the material's biological profile.
USP Class VI Compliance
Many North American OEMs specify USP Class VI as a baseline requirement. This protocol subjects plastic extracts to three in-vivo tests: systemic injection, intracutaneous reactivity and implantation.
Passing all three at the maximum extraction temperature (121 C for most medical plastics) confirms the material will not leach harmful substances under sterilization and clinical conditions. PEEK, UHMWPE, PTFE and select grades of POM and PEI all carry USP Class VI certification from their respective resin producers.
ASTM F2026: The Standard for Implant-Grade PEEK
For PEEK components intended for surgical implantation, ASTM F2026 (Standard Specification for Polyetheretherketone Polymers for Surgical Implant Applications) defines the chemical composition, mechanical property requirements, and test methods for virgin PEEK resin used in intracorporeal devices. Compliance with ASTM F2026 is a baseline expectation for any machined PEEK implant component and should be confirmed through the resin supplier's Certificate of Analysis before machining begins.
Traceability from Resin Lot to Finished Part
Biocompatibility data is only meaningful if the material in the finished part can be traced back to the tested lot. A robust traceability chain includes the resin manufacturer's Certificate of Analysis (CoA), the stock-shape converter's material certificate and the machine shop's lot record linking each finished part to the specific bar or plate from which it was cut.
Meco maintains full lot and serial traceability across all production, supported by IATF 16949:2016-certified quality management systems, PPAP documentation and CMM inspection records.
Planning a medical plastic part? Send the drawing, material requirement and target volume. Meco can review manufacturability, process fit and the quality documentation needed for the program.
Discuss Your ProjectCNC Machining vs. Injection Molding for Medical Plastics
Both processes have a place in a medical device program, and the choice depends on volume, geometry complexity and time-to-market pressure. Understanding when to machine and when to mold prevents costly tooling investments on parts that may never reach high volume, and avoids per-piece cost penalties when they do.
For a deeper explanation of the injection molding process itself, see What Is Plastic Injection Molding?
| Factor | CNC Machining | Injection Molding |
|---|---|---|
| Ideal volume range | 1 to 5,000 units per year | 5,000+ units per year |
| Tooling cost | None (fixture only) | USD 8,000 to 100,000+ depending on cavities and complexity |
| Lead time (first parts) | 1 to 3 weeks | 6 to 12 weeks (includes mold build) |
| Achievable tolerance | +/-0.025 mm | +/-0.05 mm (standard); +/-0.025 mm (precision mold) |
| Design iteration cost | Low (update CAM program) | High (mold modification or new mold) |
| Material waste | Higher (subtractive process) | Lower (near-net shape) |
| Best fit | Prototypes, verification units, bridge production, low-volume implants | High-volume disposables, housings, multi-cavity commodity parts |
Many Meco customers use a hybrid strategy: CNC-machined parts validate form, fit and function through clinical trials while the injection molding team builds production tooling in parallel. This approach compresses the overall timeline by several weeks and ensures the mold steel is cut to a design that has already been proven in patient-contact testing.
Design-for-Manufacturability Tips for Machined Medical Plastics
Polymer-specific DFM guidelines differ from those used for metals. The following practices, reviewed during every Meco quoting cycle, reduce cycle time, improve yield and prevent dimensional surprises after sterilization.
Maintain uniform wall thickness.
Abrupt changes in wall section cause uneven stress relief during and after machining. Target a minimum of 1.5 mm for most medical plastics and keep transitions gradual (3:1 taper ratio or gentler) to avoid warping after parts are removed from the fixture.
Specify tight tolerances only on critical-to-quality features.
Holding +/-0.025 mm across an entire PEEK housing adds cycle time with no functional benefit. Apply precision tolerances to mating bores, sealing faces and alignment datums; allow +/-0.05 mm elsewhere.
Account for thermal expansion.
PEEK expands at approximately 47 x 10 to the minus 6 per degree Celsius, roughly four times the rate of steel. Parts machined in a warm shop may measure undersize when inspected in a 20 C metrology lab. Whenever possible, machine and inspect in the same temperature-controlled environment.
Limit pocket depth-to-width ratios.
Keep pocket depth below 4:1 of the narrowest opening to prevent tool deflection and chatter marks that compromise surface finish. For deeper cavities, consider step-milling with progressively shorter tools.
Choose stress-relieved stock.
Extruded or compression-molded bar stock often carries internal stresses from the forming process. Annealing or stress-relief cycles before rough machining, followed by a stabilization period before finish machining, substantially reduces post-machining distortion in parts with asymmetric geometry.
Quality Assurance and Documentation for Medical Plastic Components
In the medical industrial supply chain, a part without documentation is a part without value. Meco's quality system, certified to IATF 16949:2016, provides the documentation backbone that medical OEMs and contract manufacturers need for FDA submissions and internal design history files.
The documentation package for a typical medical plastics machining order includes
- a First Article Inspection (FAI) report, which captures every dimension, tolerance and surface-finish callout from the engineering drawing and verifies them against CMM and surface profilometer data.
- A PPAP submission at Level 3 adds the control plan, Process Failure Mode and Effects Analysis (PFMEA), dimensional results, material certificates and appearance approval.
- Statistical Process Control (SPC) data with Cpk values of 1.33 or higher demonstrate ongoing process capability for repeat production lots.
- Full lot traceability links each finished part back to the raw-material CoA, the CNC program revision, the operator, the machine serial number and the inspection record.
This documentation approach does not require the machine shop itself to hold ISO 13485 certification. Many Tier 1 device manufacturers accept suppliers operating under IATF 16949 provided the supplier can demonstrate that process controls, traceability and inspection rigor meet or exceed the expectations of the device manufacturer's own quality management system.
For more detail on how these quality practices apply across all medical CNC work, see the complete guide to medical CNC machining.
Quality Documentation Checklist for Medical Plastic Programs
- IATF 16949:2016 Certified Quality System
- First Article Inspection (FAI) Reports
- PPAP Submission (Level 1 through Level 5)
- CMM Inspection Reports (+/-0.002 mm precision)
- Material Certificates with full CoA and resin lot traceability
- Process Control Plans with CTQ identification
- PFMEA (Process Failure Mode and Effects Analysis)
- SPC Data with Cpk values of 1.33 or higher
- Full Lot and Serial Traceability
- REACH and RoHS Compliance Documentation
What to Look for in a Medical Plastics Machining Partner
Selecting the right contract manufacturer determines whether a plastic medical component reaches market on time, on spec and with audit-ready documentation. The criteria below reflect what experienced procurement and quality teams evaluate when qualifying a supplier.
Polymer-specific machining experience.
Cutting PEEK is not the same as cutting aluminum. Look for a partner that can demonstrate proven programs in at least three medical-grade polymers, with sample parts, tolerance studies and surface-finish data to back the claim.
Multi-process capability.
A device program rarely involves only machined plastics. If the same supplier can also deliver CNC-machined metal components, injection-molded housings, surface finishing and mechanical assembly, the device manufacturer eliminates multiple vendor qualifications, reduces freight touches and compresses lead times.
Meco's integrated capabilities span CNC machining, injection molding, metal stamping, die casting, forging, welding, surface treatment and box-build assembly.
Scalability without minimum order quantities.
Medical programs evolve from single prototypes through pilot runs of 50 units to annual volumes of tens of thousands. Meco supports orders from one piece to more than 10 million with no MOQ, maintaining the same quality system at every volume level.
Global logistics and local warehousing.
Meco operates manufacturing facilities in Thailand (20,000 square meters) and China (16,000 square meters), with warehousing and fulfillment hubs in the United States, Canada, Japan and Thailand. This footprint allows just-in-time delivery to North American OEMs while leveraging cost-effective production in Asia.
For a broader view of how CNC machining, assembly and packaging come together in a turnkey medical program, read the article on medical device assembly automation.
Discuss your medical plastic part
Share the drawing, material requirement, target volume and any documentation requirements. Meco can review the machining approach and identify where manufacturing or inspection choices need to be clarified before production.
- DFM. Engineering feedback with the quote.
- Scale. No minimum order, from prototypes to production.
- Quality. IATF 16949:2016 certified, with FAI, PPAP and CMM reporting available.
- Traceability. Material certificates and full process records available.
- Confidentiality. NDA available before drawings or files are shared.
Browse CNC machining capabilities or review the medical CNC machining guide.
Talk to an EngineerReferences and sources
Standards and regulatory references in this article were reviewed for this update.
- International Organization for Standardization. ISO 10993-1:2025, Biological evaluation of medical devices, Part 1. Published 2025.
- U.S. Food and Drug Administration. Use of International Standard ISO 10993-1. Guidance for Industry and FDA Staff, September 2023.
- ASTM International. ASTM F2026-23, Standard Specification for PEEK Polymers for Surgical Implant Applications. Current ASTM standard page.
