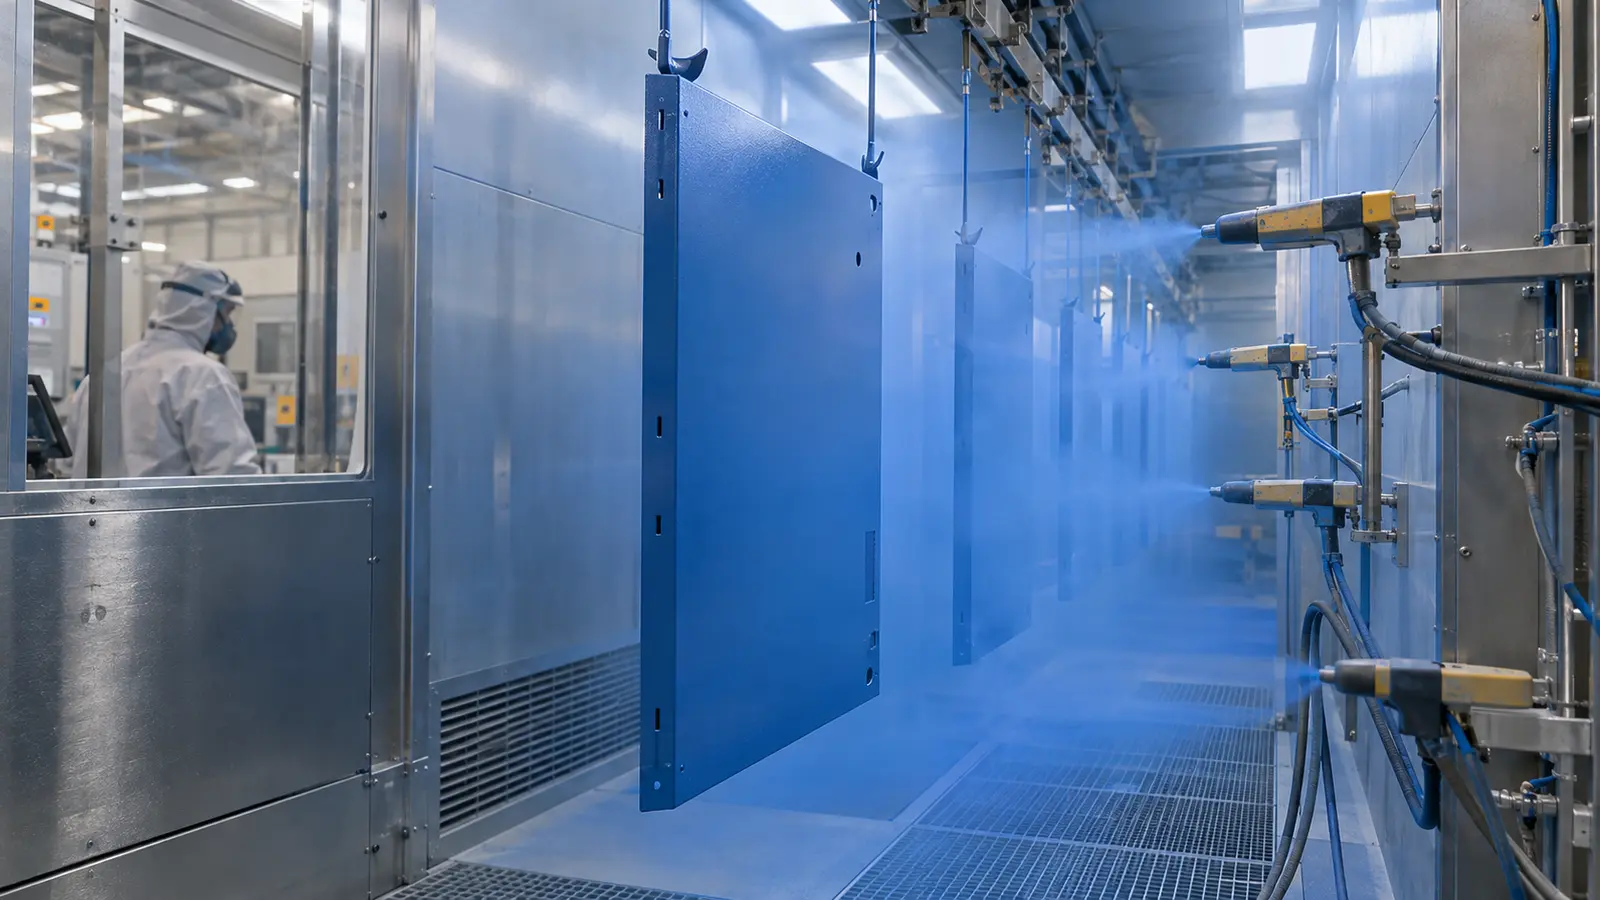
For high-volume manufacturing, powder coating commonly costs about $0.50 to $2.50 for small parts, $5 to $15 for medium assemblies, and $20 or more for large structures.
The final unit price depends on rack density, pretreatment, masking, powder type, colour changes, inspection and production volume. These are planning ranges, not quotations.
The correct comparison is total landed cost per accepted part, including freight, handling, rework and supplier handoffs.
Powder coating does not have one reliable per-part or per-square-foot price for industrial production. A shop must price the part geometry, the coating specification and the way each item moves through the line.
A low spray price can become expensive when masking is manual, parts travel between several vendors or the finish must be reworked. This guide explains the cost structure used for OEM budgeting and supplier comparison.
For broader finish selection, see Meco's surface finishing services. If the substrate must be mechanically prepared first, review the sand-blasted finish guide.
Key takeaways
- Small production parts may fall near $0.50 to $2.50 each, while larger or labour-intensive parts can cost much more.
- Rack density, masking and pretreatment often influence price more than the powder itself.
- Powder recovery and fast thermal curing can make powder coating efficient for repeat production.
- Powder coating hides minor surface variation better than transparent anodizing, but it also adds film thickness.
- Combining fabrication, finishing and inspection reduces freight, handling and accountability gaps.
How Much Does Powder Coating Cost in 2026?
Industrial powder coating prices vary mainly by part size, handling time and batch efficiency. The ranges below are useful for feasibility work when the design is still being defined.
| Part group | Examples | Planning range | Typical cost sensitivity |
|---|---|---|---|
| Small components | Brackets, clips and stampings | $0.50 to $2.50 per part | Rack density and masking |
| Medium assemblies | Electronic enclosures and chassis | $5 to $15 per part | Surface area, colour and handling |
| Large structures | Equipment housings and frames | $20 or more per part | Booth and oven capacity, lifting and coverage |
Why quotes differ
Two parts with the same surface area can have different costs. A simple bracket may hang densely on a rack, while an enclosure with protected threads, cosmetic faces and internal corners needs more labour and line space.
What Drives Powder Coating Cost?
The largest cost drivers are line density, pretreatment, masking, powder selection, colour change and quality requirements. Each one changes labour, material use, equipment time or risk.
| Cost driver | Why it changes price | What the buyer can define |
|---|---|---|
| Rack density | More parts per rack spread line time across more units | Stable hanging points, spacing and protected contact areas |
| Pretreatment | Cleaning, rinsing and conversion stages add process time and chemistry | Substrate condition and required corrosion performance |
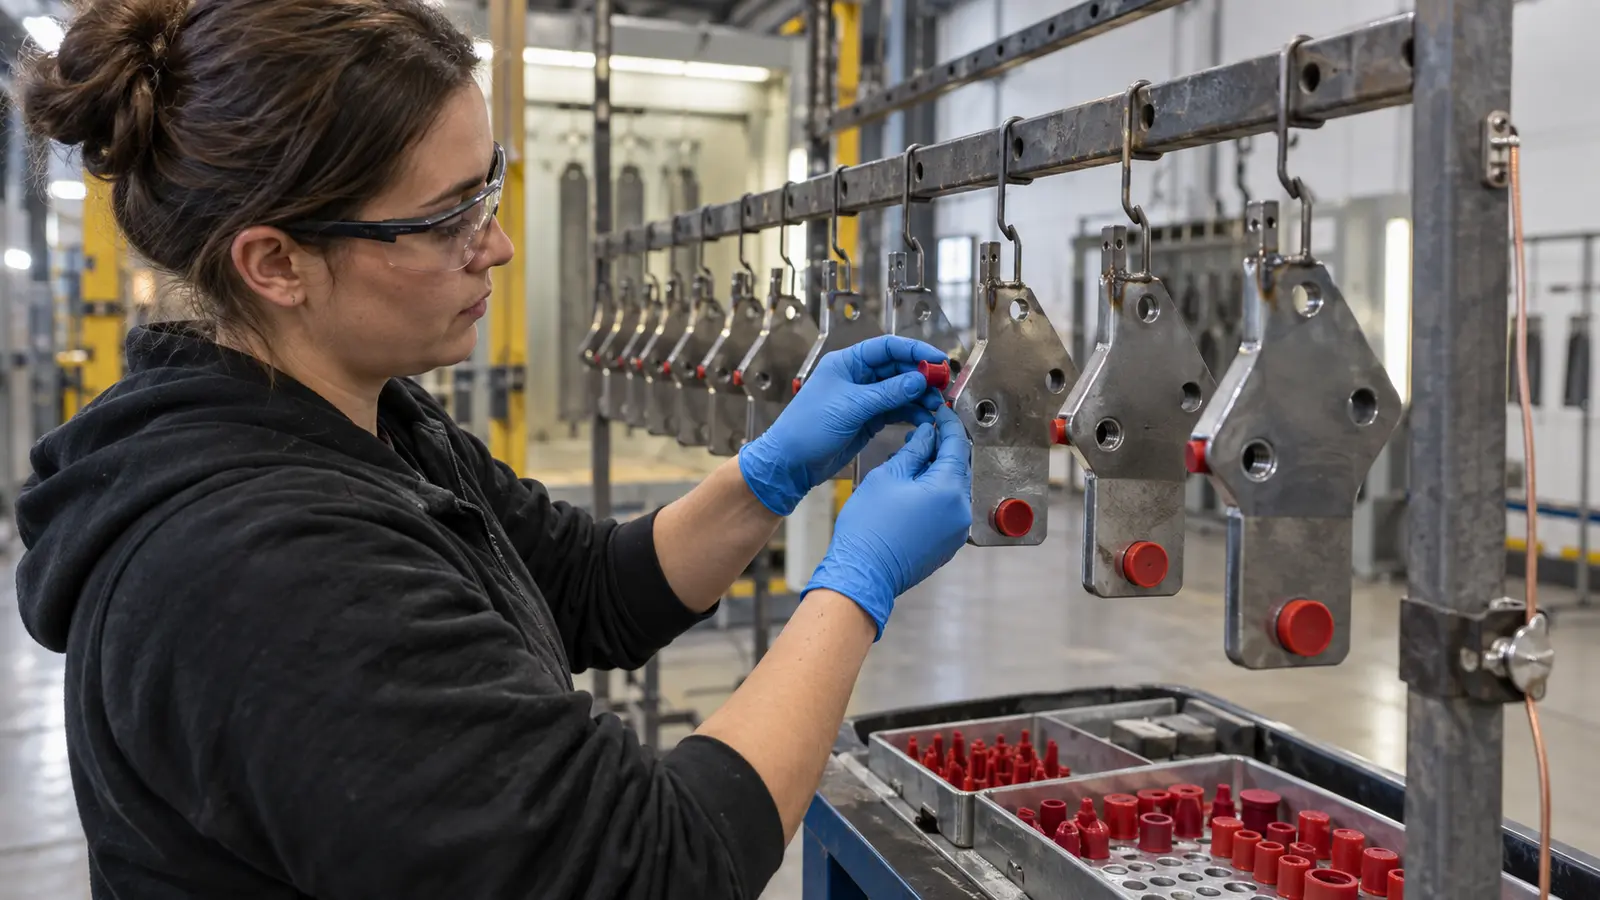
| Masking | Threads, bores, grounds and mating faces may need manual plugs or tape | A masking drawing and reusable mask strategy |
| Powder system | Resin, texture, gloss and special approvals affect material and process control | Environment, colour, gloss, texture and performance standard |
| Colour change | Booth and gun cleaning creates downtime between colours | Standard colours, forecast and batch sequence |
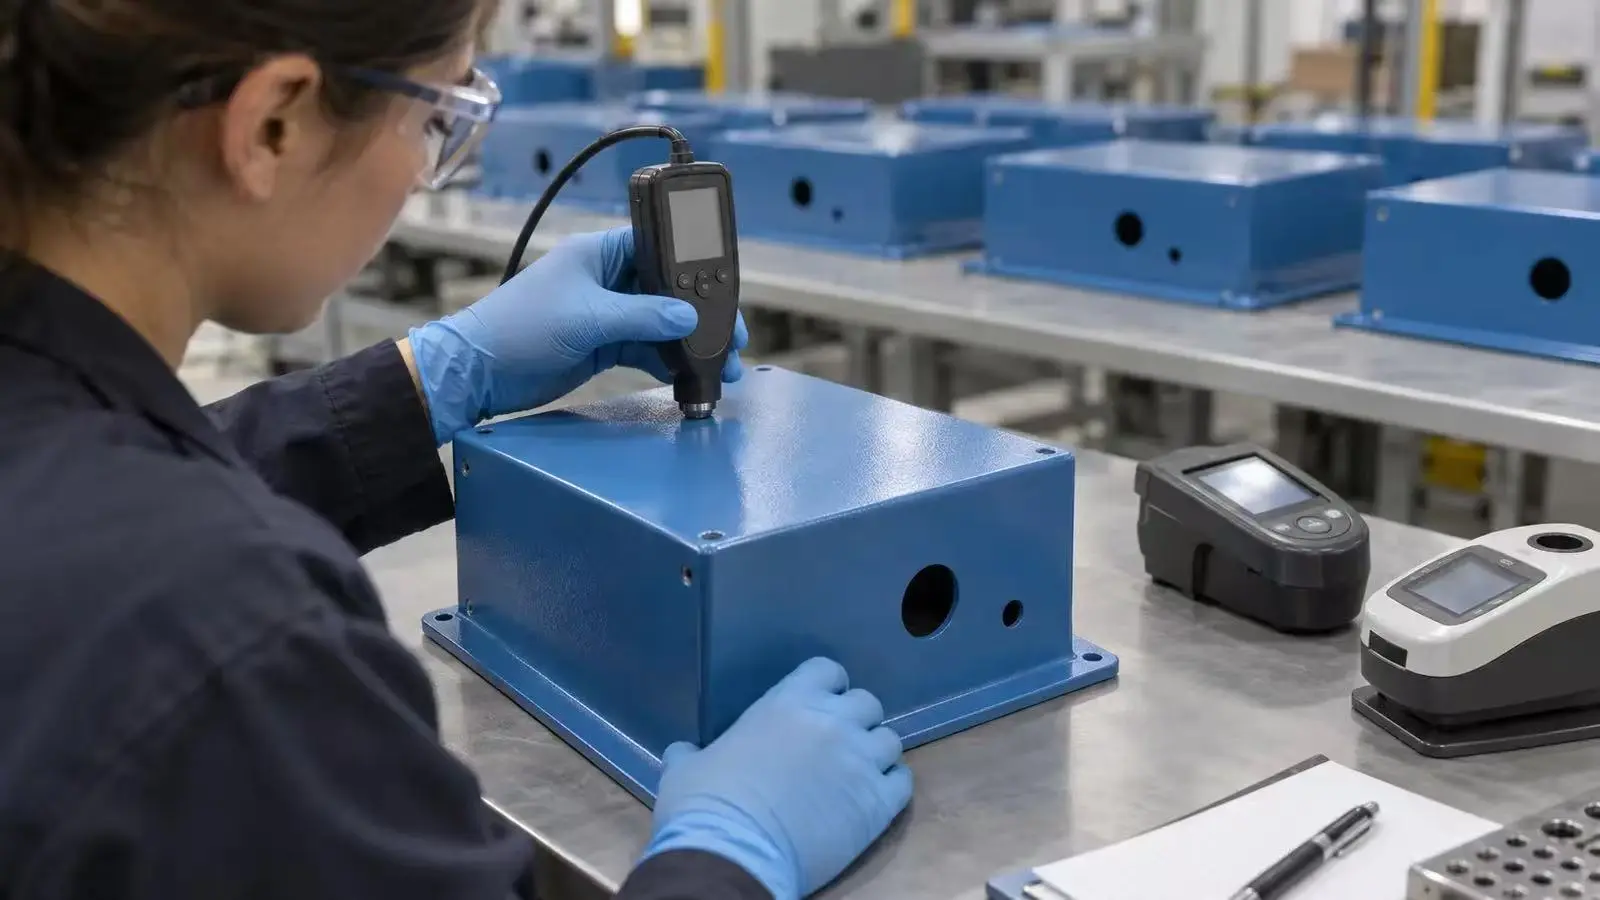
| Inspection | Thickness, colour, gloss, adhesion and corrosion checks require equipment and records | Acceptance criteria, sample rate and report format |
Volume and rack utilisation
A repeat order spreads line setup and colour-change time over more parts. Geometry still matters. Parts that shadow one another or trap powder need more spacing and careful gun access.
Masking and manual labour
Masking can cost more than the powder on a precision assembly. Identify threads, electrical grounds, bearing seats, sealing surfaces and critical fits on the drawing. Reusable silicone caps and dedicated fixtures may justify their cost on repeat programmes.
Pretreatment and substrate condition
Powder must be applied to a clean and properly prepared surface. Oil, oxide, scale, weld residue and casting contamination change the required preparation route. A quote should state whether cleaning, blasting or conversion coating is included.
Powder chemistry and appearance
Epoxy systems suit many indoor chemical-resistance applications, while polyester systems are common where outdoor colour and gloss retention matter. Special textures, metallic effects, approved powder systems or exact colour matching can increase material and changeover cost.
Which Process Steps Are Included?
A complete quote should cover receiving, preparation, masking, racking, spraying, curing, cooling and inspection. Packaging may be separate, so confirm where responsibility begins and ends.
- Review. Confirm substrate, drawing, finish code, colour, gloss and protected features.
- Prepare. Remove oil and contamination, then apply the specified mechanical or chemical pretreatment.
- Mask and rack. Protect functional surfaces and orient parts for coating coverage and grounding.
- Apply powder. Electrostatic guns deposit the specified powder while the booth controls overspray.
- Cure. The coating flows and cross-links under the time and temperature schedule required by the powder supplier.
- Inspect and pack. Check film, appearance and required tests before protecting finished surfaces for shipment.
Meco's production resources include an automated powder coating line, Gema spray technology, ceramic pretreatment, powder and paint thickness measurement, spectrophotometry, gloss measurement and salt-spray testing. The required checks should still be written into the purchase specification.
Powder Coating vs Wet Paint vs Anodizing
Powder coating is often the production choice for durable coloured metal parts, but it is not automatically right for every tolerance or appearance requirement. Wet paint offers thin films and field touch-up options, while anodizing changes the aluminum surface itself.
| Selection factor | Powder coating | Wet paint | Anodizing |
|---|---|---|---|
| Compatible substrates | Conductive metals that tolerate the cure cycle | Broad material range, including heat-sensitive parts with the right system | Aluminum and selected nonferrous alloys |
| Film and appearance | Thicker coloured film that can soften minor surface variation | Thin to medium film with broad colour and touch-up options | Integral oxide layer that keeps the metal texture visible |
| Production efficiency | Strong for repeat line work and recoverable overspray systems | May require solvent controls and longer handling before full cure | Batch chemistry with careful alloy and cosmetic control |
| Design caution | Allow for coating thickness on fits, threads and grounds | Control runs, edge coverage and solvent compatibility | Base-metal marks and alloy variation remain visible |
For machined aluminum, surface roughness and tool marks affect the visible result. Use the surface finish chart to define only the areas that need a tighter Ra target.
How Can You Reduce Powder Coating Cost?
The best savings come from reducing manual handling and making the specification complete before production begins. A design review can remove masking, colour changes and rework without weakening the performance requirement.
- Use standard colours and powder systems when appearance permits.
- Add reliable hanging and grounding points that do not affect cosmetic surfaces.
- Mark every masked thread, bore, mating face and electrical ground on the drawing.
- Use reusable plugs or fixtures for stable repeat volumes.
- Batch similar colours and substrates to reduce booth cleaning and line changes.
- Set measurable film thickness, colour, gloss and cosmetic acceptance criteria.
- Design packaging around cured surfaces, edges and cosmetic faces.
Need a coating-ready review? Send the CAD model, drawing, substrate, colour, annual volume and finish specification. Meco will review masking, hanging, pretreatment and inspection before quoting.
Get DFM Feedback on Your DesignWhy Total Landed Cost Matters
A separate coating vendor adds freight, packaging, queue time, incoming inspection and another handoff. Those costs may not appear in the coating line item, but they still affect the delivered part.
A die-cast or fabricated housing may move through machining, cleaning, coating and assembly. When separate suppliers control each step, a finish defect can trigger a long investigation into casting release agent, machining coolant, pretreatment or cure. One accountable manufacturing partner can control the route and the corrective action.
| Cost category | Budget finish example | Controlled powder finish example |
|---|---|---|
| Finish price | $2.00 per part | $2.50 per part |
| Upfront finish cost | $20,000 | $25,000 |
| Assumed field claims | 300 at $150 each | 20 at $150 each |
| Illustrative total | $65,000 | $28,000 |
The point is not the assumed failure rate. The useful method is to compare finish price with expected rework, warranty handling, replacement freight and service labour. Replace every assumption with programme data before making a sourcing decision.
What Should You Send for a Powder Coating Quote?
A complete quote package defines the part, finish, volume and acceptance criteria. It prevents suppliers from pricing different assumptions and makes proposals easier to compare.
- 3D CAD and a controlled 2D drawing
- Substrate material and current surface condition
- Part dimensions, weight and annual volume
- Powder manufacturer, product code or performance specification if required
- Colour standard, gloss range and texture
- Film-thickness range and any cure restrictions
- Masking map for threads, grounds, bores, seals and mating surfaces
- Pretreatment and corrosion requirements
- Cosmetic zones, defect limits and approved sample process
- Inspection reports, traceability, packaging and delivery location
If the project also includes casting, machining, fabrication or assembly, ask for one process map and one delivered price. Meco's whole-product manufacturing model is designed for programmes where the finish must be controlled with the part, not purchased as an isolated step.
Quote the Finished Part
Meco can review the complete route from fabrication and machining through pretreatment, powder coating, inspection, assembly and delivery.
- Response. Quote review within 24 hours.
- Engineering. DFM feedback with every quote.
- Process. Automated powder coating with controlled pretreatment and inspection.
- Quality. IATF 16949:2016 with FAI, PPAP and CMM reporting available.
- Scale. Prototype support through mass production.
Browse all 40+ processes, review surface finishing options, or go straight to a quote.
Request a Quote Today