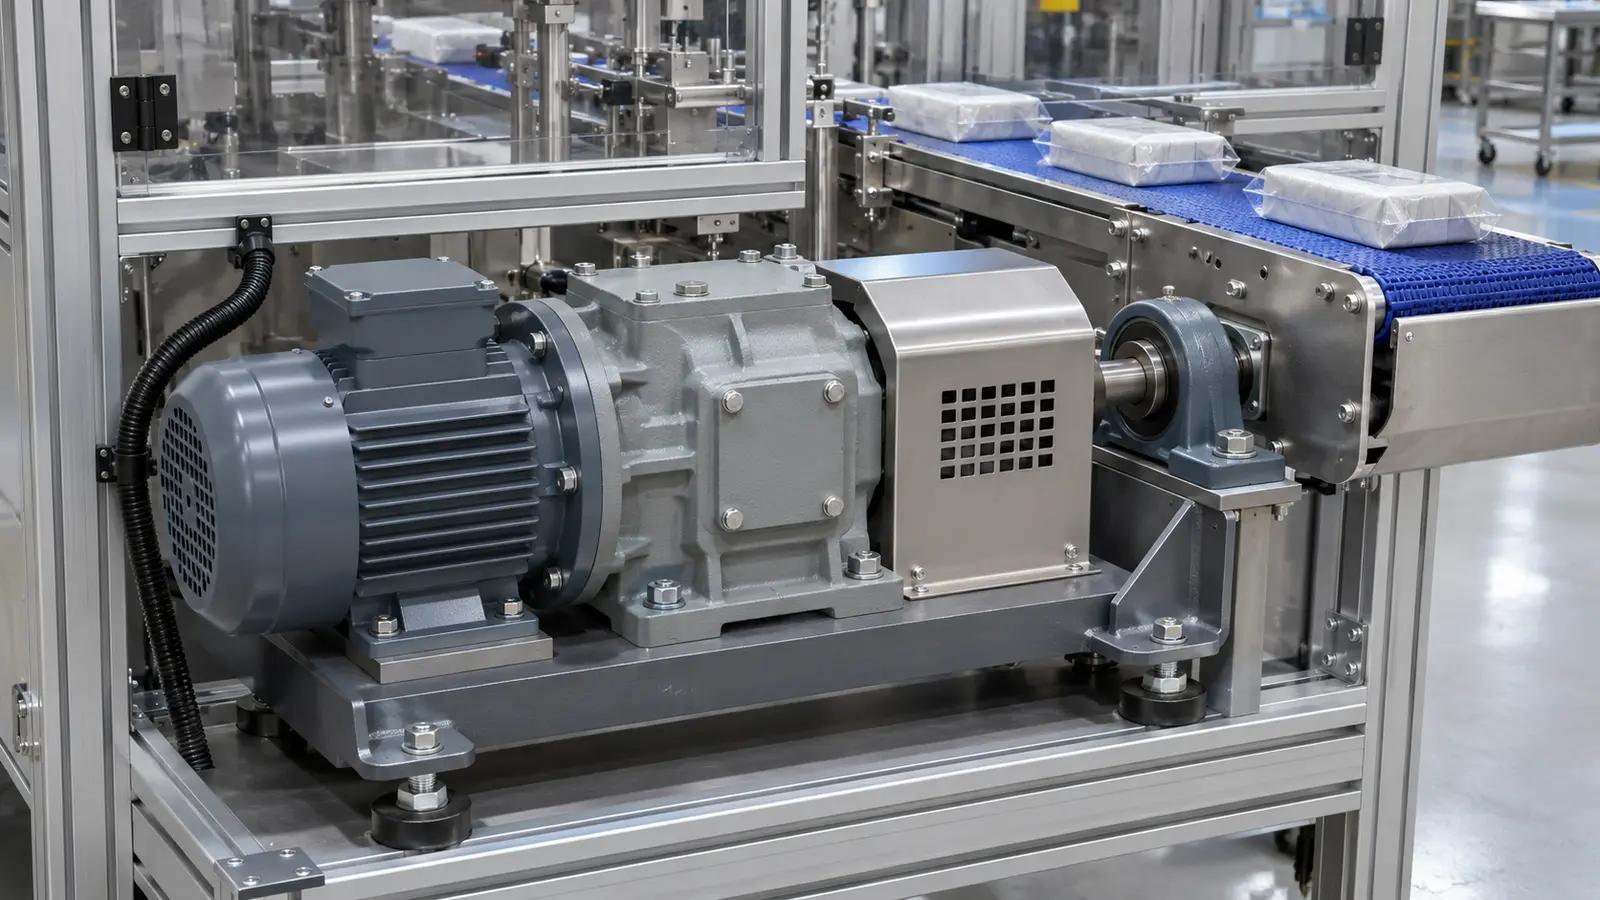
Mechanical assembly joins separately manufactured components into a working subassembly or finished product using controlled fastening, pressing, riveting, welding or other joining methods.
For OEMs, reliable assembly depends on part fit, tolerance stack-up, the chosen joining process, finish compatibility and clearly defined inspection and test requirements.
Mechanical assembly is the process of joining individual components into a functional subassembly or finished product using controlled methods such as fastening, riveting, press-fitting, welding, adhesive application, and electromechanical integration. In OEM manufacturing, it is not just a final production step. It is where part quality, tolerance control, process discipline, and supply chain coordination determine whether a product launches smoothly or creates costly rework.
For North American OEMs, that matters because assembly issues are rarely isolated. A misaligned bracket, damaged coating, unmanaged tolerance stack-up, or inconsistent torque value can delay production, increase warranty exposure, and disrupt delivery. That is why companies searching what is mechanical assembly are usually not looking for a simple definition. They want to understand how the process works, where it fits in turnkey manufacturing, and how to choose a supplier that can do it reliably at scale.
Key Takeaways
- Mechanical assembly turns separate parts into a working product. It combines machined parts, castings, plastics, fasteners, seals, and electronics into one repeatable final build.
- Assembly quality depends on more than labor. Tolerance control, fixturing, torque management, cleaning, coating compatibility, and inspection all affect the finished product.
- The assembly of machined parts requires extra control. Burrs, surface contamination, thread quality, and tolerance stack-up can all affect fit and function after machining is complete.
- Assembly and coating services work best when planned together. Finishes such as anodizing, zinc plating, and powder coating affect corrosion resistance, fit, cosmetic quality, and downstream assembly performance.
- Turnkey manufacturing reduces risk. When one partner manages machining, finishing, assembly, packaging, and logistics, OEMs gain better accountability, faster communication, and fewer quality gaps.
What Is Mechanical Assembly?
Mechanical assembly is the controlled process of bringing manufactured components together so they function as one finished system. Those components may include machined metal parts, castings, molded plastics, fasteners, bearings, seals, springs, wiring, and electronics.
At a technical level, mechanical assembly involves much more than putting parts together. It requires revision-controlled BOMs, fixture-based alignment, fastening control, material compatibility planning, in-process inspection, and functional verification. That is why strong mechanical assembly services are closely tied to engineering support and upstream manufacturing quality.
In modern OEM production, mechanical assembly often includes:
- subassembly build
- final assembly
- electromechanical integration
- torque-controlled fastening
- quality inspection and documentation
- packaging and shipment preparation
If you want to see how assembly fits into a larger manufacturing model, explore Meco’s whole product manufacturing solution.
Why Mechanical Assembly Matters in OEM Manufacturing
Mechanical assembly matters because it is the point where part-to-part variation becomes visible. A component can meet print on its own and still create problems in the final build if tolerances accumulate across the product or if the joining process is inconsistent.
For OEMs, those problems can show up as:
- fit issues during launch
- misalignment and vibration problems
- inconsistent torque or preload
- cosmetic defects
- field-service failures
- higher scrap and rework costs
According to NIST research on electro-mechanical assemblies, tolerance analysis and tolerance allocation play a direct role in assembly performance and manufacturability. That means assembly quality is tied to design and dimensional variation management, not just line-side labor execution. NIST reference .
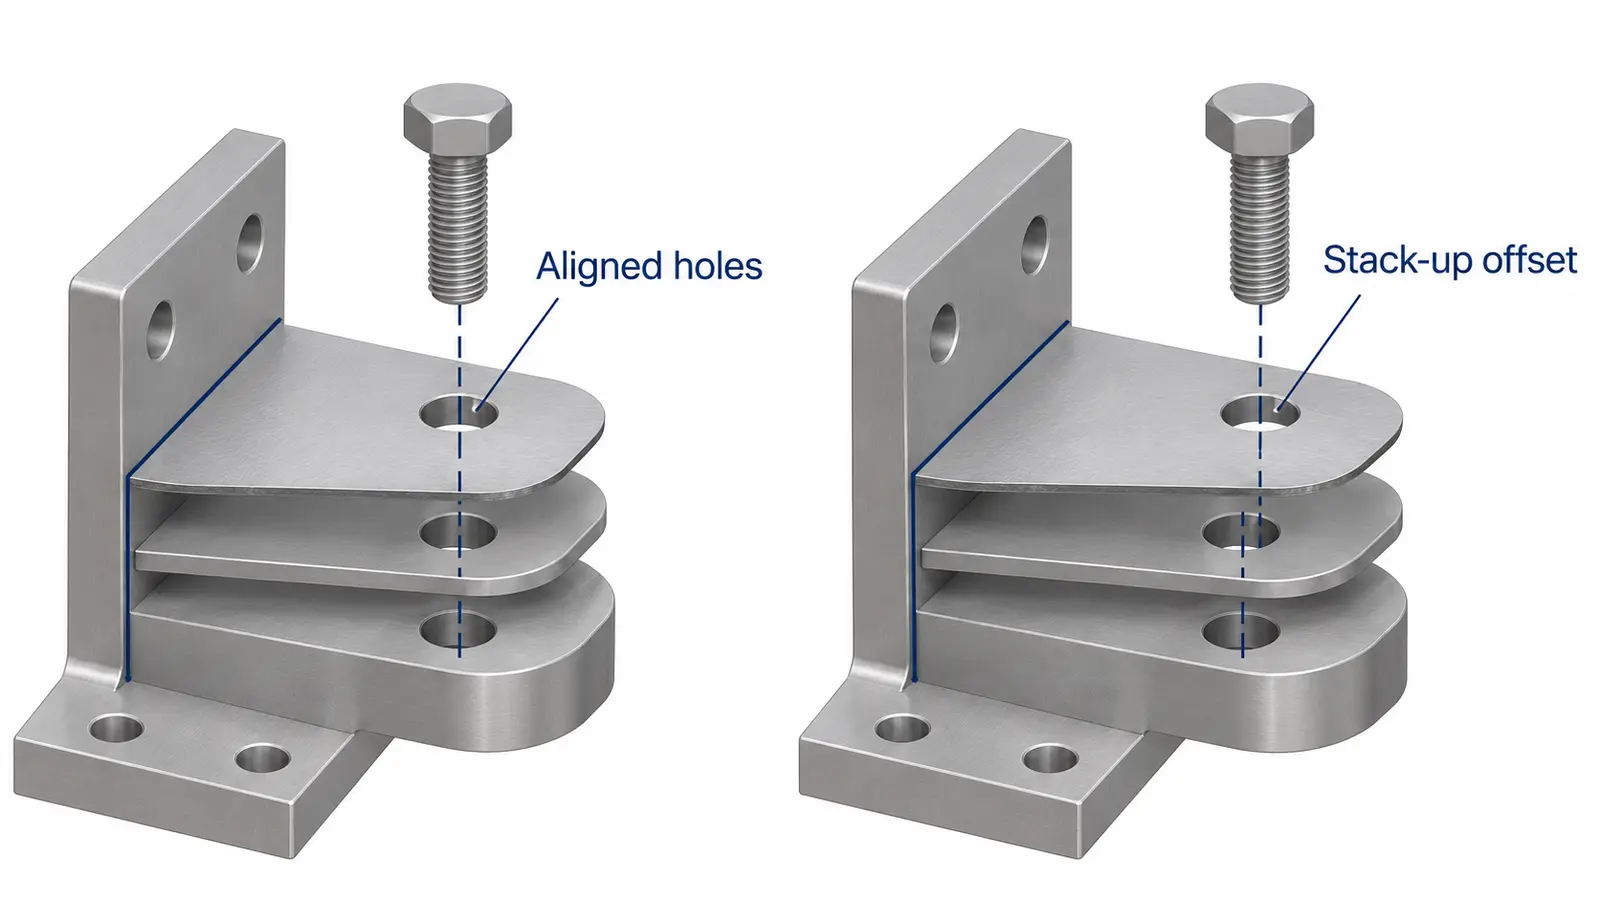
That is why OEMs often prefer suppliers that connect assembly to upstream custom CNC machining, injection molding, die casting and surface finishing, rather than treating each handoff as a separate problem.
How Does the Mechanical Assembly Process Work?
Mechanical assembly works by moving components through a controlled sequence that ensures alignment, joint integrity, inspection, and functional performance. While the exact workflow depends on the product, most OEM programs follow a similar structure.
1. Design review and assembly planning
Before production starts, engineering teams review drawings, material requirements, assembly sequence, fastening methods, finish requirements, testing criteria, and packaging needs. This is where DFM and DFA improvements can reduce labor time, remove unnecessary components, and prevent tolerance-related issues.
Meco’s R&D engineering support helps customers address manufacturability and assembly risk before production ramps.
2. Incoming part verification
Components are checked for dimensional conformity, surface condition, thread quality, finish quality, and lot traceability. If a part is out of spec, assembly should not proceed until the issue is contained.
3. Cleaning and preparation
Preparation may include deburring, cleaning machining residue, applying lubricant, preparing adhesives, masking critical surfaces, and kitting components by work order. This is especially important when the product includes precision-machined or coated parts.
4. Alignment and fixturing
Fixtures, jigs, locating pins, and stops keep parts in the correct relationship during joining. Without reliable fixturing, repeatability drops and tolerance stack-up becomes harder to control.
5. Joining and fastening
Depending on the design, joining may include automatic screwdriving with torque control, orbital riveting, pull riveting, press-fit assembly, shrink fitting, adhesive dispensing, welding, or electromechanical integration. Meco’s mechanical assembly services support both mechanical and electromechanical programs, including ESD-safe environments for electronics-related builds.
6. Inspection and verification
In-process and final verification may include dimensional checks, torque validation, visual inspection, functional tests, traceability confirmation, and documentation such as PPAP, FAI, CMM reports, and COA.
7. Packaging and logistics readiness
A turnkey assembly workflow does not end at the workstation. Final steps may include custom packaging, labeling, lot coding, kitting, warehousing, and delivery planning through warehousing and fulfillment services and supply chain management .
What Are the Main Types of Mechanical Assembly?
Mechanical assembly includes several joining and build strategies depending on part geometry, material mix, service requirements, and production volume.
A sub-assembly is a module that will later be installed into a larger product; final assembly produces the complete deliverable. This distinction helps define handoffs and test responsibilities.
Fastener-based assembly
Fastener-based assembly uses screws, bolts, nuts, threaded inserts, clips, and similar hardware to create joints that are often serviceable. This method is common because it supports maintenance, field repair, and design iteration.
Fasteners often create removable joints, making them useful when a product must be serviced, inspected or revised. The selected hardware still needs defined preload and locking requirements.
Riveted assembly
Riveting is used where permanent mechanical joining is needed with strong repeatability. It is common in sheet metal, lightweight structures, and applications where back-side access is limited.
Press-fit and interference-fit assembly
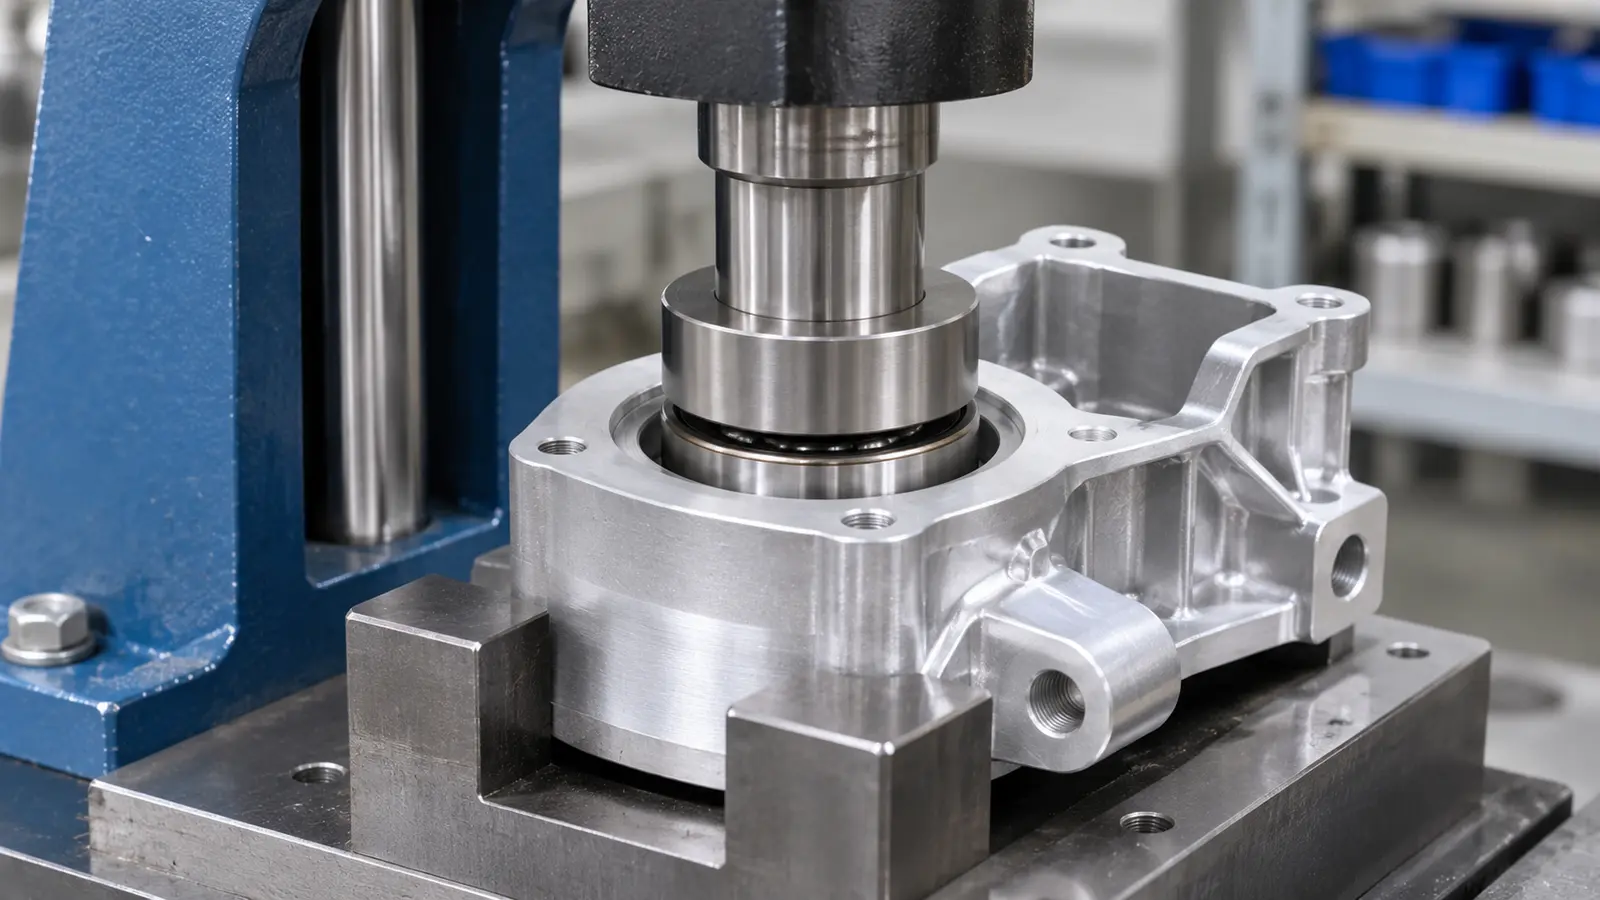
Press fits rely on controlled interference between mating parts such as bearings, bushings, shafts, and pins. Successful press-fit assembly depends on chamfers, insertion force control, alignment, cleanliness, and material behavior.
Clean fit surfaces, suitable lead-ins, correct alignment and controlled installation force all support repeatable press fits. JTEKT bearing mounting guidance also explains why pressing force must act on the ring being fitted rather than passing through rolling elements.
Welded assembly
Welding creates permanent joints and is common in structural frames, fabricated housings, heavy equipment parts, and brackets. In turnkey programs, welding often connects directly to custom laser cutting services , CNC bending , and TIG welding .
Adhesive-assisted assembly
Adhesives can improve sealing, vibration damping, and mixed-material compatibility. They must still be managed carefully for cure time, surface preparation, and environmental exposure.
Electromechanical assembly
Many OEM products combine metal parts, plastics, PCBAs, connectors, harnesses, and sensors. In those cases, assembly must also account for ESD protection, cable routing, connector retention, thermal management, and final test requirements. Related reading: What Is Box Build Assembly?
What Is the Assembly of Machined Parts?
The assembly of machined parts is the process of joining precision-machined components into a finished subassembly or final product while maintaining alignment, fit, torque, and functional performance. In OEM manufacturing, this requires much more than accurate machining alone.
Machined components are often assembled with pins, bearings, bushings, fasteners, seals, castings, molded parts, or electronics. That is why a strong assembly partner must understand not only part accuracy, but also how those dimensions behave once multiple features come together in the final build.
Why machined-part assembly is more demanding than it looks
A machined component may meet print and still create issues at assembly if the process is not controlled. Burrs, contamination, thread damage, and tolerance stack-up can all affect final performance once multiple parts are joined.
For that reason, the assembly of machined parts often includes:
- incoming dimensional verification
- deburring and cleaning
- fixture-based positioning
- controlled torque application
- press-fit or interference-fit validation
- in-process inspection
- functional testing before pack-out
If your product includes shafts, housings, brackets, threaded features, or precision mating surfaces, assembly planning should begin during design, not after machining is complete. This is where R&D engineering and DFM feedback help reduce avoidable rework.
Common examples of machined-part assemblies
Typical OEM examples include:
- gearbox housings with bearings, seals, and fasteners
- aluminum enclosures with inserts and covers
- machined brackets assembled to stamped or molded parts
- valve bodies with threaded fittings and precision bores
- electromechanical products that combine machined metal parts with PCBAs
For more complex geometry or tighter positional control, manufacturers may combine assembly with 5-axis CNC machining , CNC turning services , or CNC milling service capabilities before final build.
Best practices for assembly of machined parts
A robust machined-part assembly process focuses on tolerance control across mating parts, repeatable fixturing, proper joining method selection, traceable inspection records, and a smooth transition from prototype builds to volume production.
When OEMs use separate suppliers for machining and assembly, they often lose time diagnosing fit problems between processes. An integrated workflow reduces that gap by giving one partner accountability for both part quality and final build quality.
What Are Assembly and Coating Services?
Assembly and coating services combine product assembly with protective or cosmetic finishing so parts arrive ready for installation, shipment, or end use. Instead of sending components to separate suppliers for finishing and then assembly, OEMs can coordinate the workflow through one manufacturing partner.
This matters because coatings do more than improve appearance. They affect corrosion resistance, wear life, electrical behavior, part fit, and cosmetic acceptance. When assembly and coating are planned together, manufacturers can reduce handling damage, shorten lead times, and improve consistency from part production through final delivery.
Why assembly and coating should be planned together
A coating can change how parts fit, how threads engage, and how surfaces behave in service. For example:
- anodizing affects aluminum surface characteristics and wear resistance
- zinc plating protects steel against corrosion
- powder coating adds durable coverage but requires cure-temperature compatibility
- painting and e-coat can affect masking strategy, mating surfaces, and cosmetic quality
ASTM B633-23 establishes requirements for electrodeposited zinc coatings on iron and steel used for corrosion protection. The ASTM B633-23 standard overview describes its scope.
MIL-PRF-8625 is an active U.S. specification for anodic coatings on aluminum and aluminum alloys. Review the official specification record when a drawing names this requirement.
For OEMs, this means coating decisions should be made before release to production, especially when assemblies include threaded holes, press fits, grounding points, sealing surfaces, cosmetic faces, and mixed-material interfaces. This is exactly why Meco integrates surface finishing services with upstream manufacturing and downstream assembly.
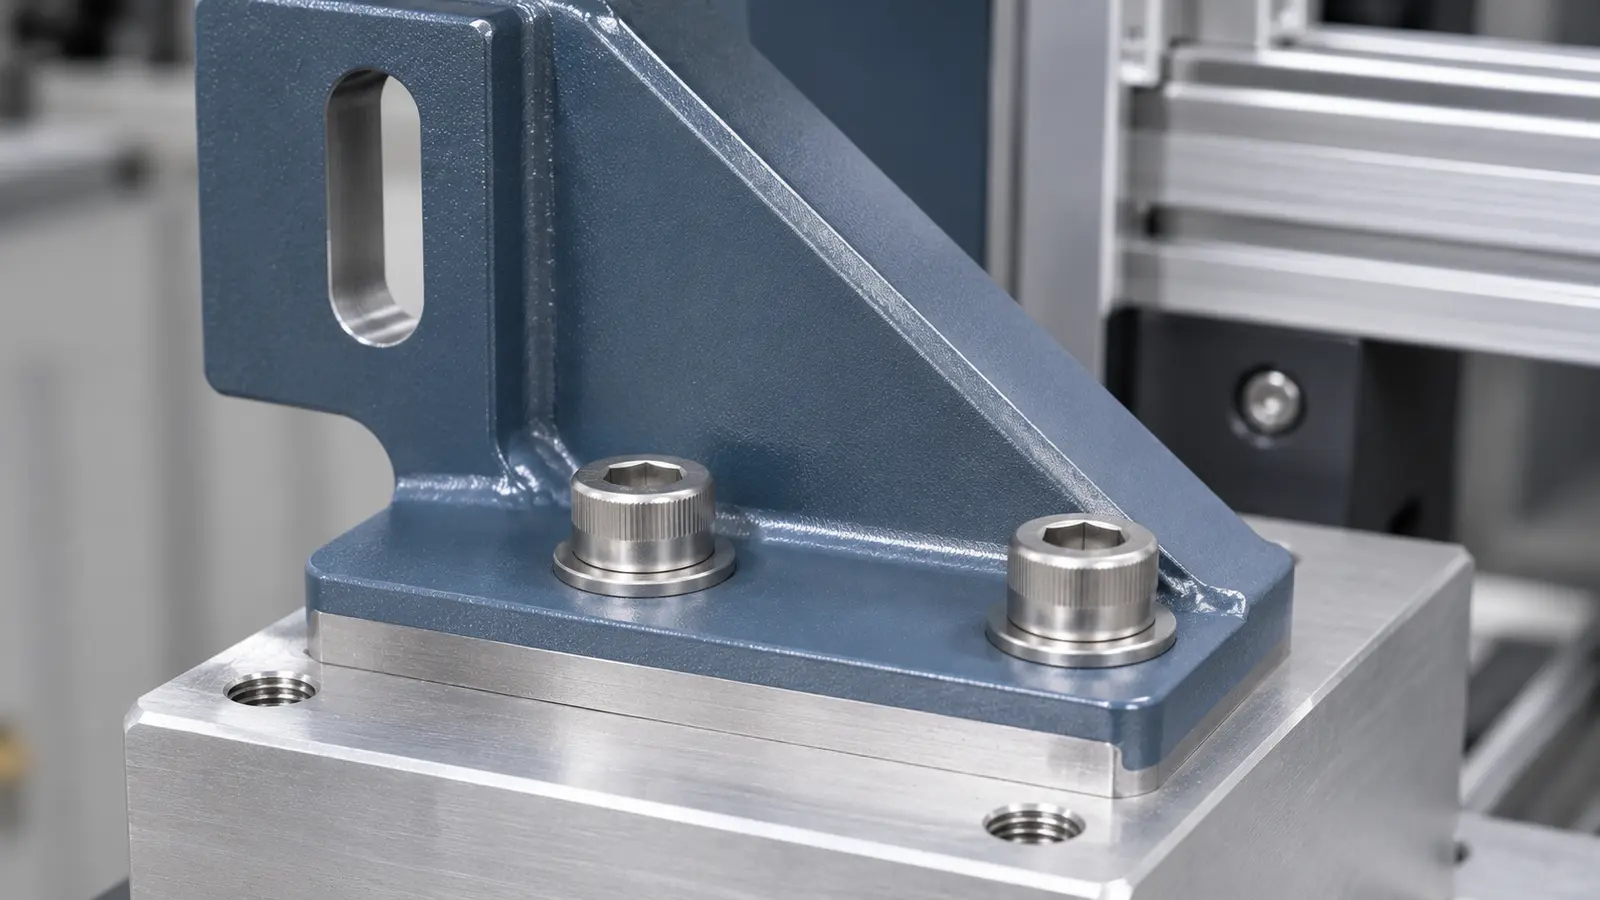
Where assembly and coating services add the most value
Assembly and coating services are especially valuable when products include multiple fabricated or machined metal parts that must be delivered as one finished unit. Typical examples include:
- welded frames that need powder coating after fabrication
- machined aluminum housings that require anodizing before final build
- zinc-plated steel brackets joined with appropriate fasteners after finishing
- consumer-facing products where finish quality and fit must both be controlled
The biggest benefit is operational. One partner can coordinate masking requirements, coating sequence, cure-temperature compatibility, post-finish inspection, final assembly, and packaging. That reduces supplier handoffs and lowers the risk of finish damage during transport between vendors.
How Meco approaches assembly and coating services
Meco supports integrated workflows that combine machining, fabrication, finishing, and final assembly so products can move through fewer suppliers and fewer quality breakpoints. Depending on substrate and application, finishing options include anodizing, zinc plating, nickel plating, electroless nickel, PVD, painting, powder coating, e-coating, and galvanizing through our surface finishing services capability.
If your program also requires fabrication before finishing, related capabilities include custom laser cutting services , CNC bending , and TIG welding . For a broader technical overview of finishing processes, see Nordson’s powder coating guide .
Planning a multi-part assembly? Send the drawings, BOM and finish requirements. Meco can review joint choices, build scope and practical manufacturing constraints before quoting.
Talk to an EngineerMechanical Assembly and Other Joining Approaches
Fastener-based mechanical assembly is a common choice because it can support serviceability and mixed-material products. Welding, bonding and molding-based joining may also be appropriate within a larger assembly workflow, depending on the joint and the product.
| Joining Method | Main Advantage | Main Limitation | Best Fit |
|---|---|---|---|
| Fastener-based assembly | Serviceable, flexible, good for mixed materials | Requires hardware or controlled joining process | Products needing repair, modularity, or design iteration |
| Welding | Very strong permanent joints | Heat distortion, no disassembly | Frames, structural weldments, heavy-duty assemblies |
| Adhesive bonding | Clean surfaces, useful for dissimilar materials | Cure time and surface prep sensitivity | Sealing, damping, cosmetic assemblies |
| Overmolding | Integrated high-volume solution | High tooling commitment, less flexibility for changes | Consumer products and sealed housings at scale |
Fastener-based assembly is often preferred when the product needs maintenance access, replaceable parts, controlled torque or design flexibility during ramp-up. For broader outsourcing scope, read the guide to contract assembly .
Which Industries Rely on Mechanical Assembly?
Mechanical assembly is used across nearly every sector, but requirements differ by industry.
Automotive
Automotive programs rely on tight tolerances, repeatable fastening, traceability, and scalable throughput. Explore automotive parts manufacturing .
Aerospace
Aerospace assembly programs may involve lightweight metals, full traceability, first article inspection records and customer-specific approval requirements. See Meco’s aerospace parts manufacturing capabilities for applicable process options.
Industrial equipment
Industrial products often require rugged subassemblies, welded structures, machined housings, and serviceable builds designed for long life in harsh environments. Explore industrial manufacturing .
Consumer electronics
Consumer and electronics products often combine metal, plastic, connectors, PCBAs, and cosmetic finishes. Explore custom electronics manufacturing .
Medical equipment
Medical equipment assemblies require reliability, documentation, cleanliness, and traceability. Explore medical equipment manufacturing .
What Are the Main Benefits of Mechanical Assembly?
Mechanical assembly offers OEMs a combination of precision, flexibility, and scalability that few joining methods can match across multiple industries.
- Serviceability for products that need field repair or replacement
- Multi-material compatibility across metals, plastics, castings, and electronics
- Faster design iteration during prototype and ramp-up stages
- Better integration with turnkey manufacturing through one accountable partner
- Scalable production from pilot runs to volume manufacturing
- Stronger quality control and traceability across joining, inspection, and logistics
How Do You Choose the Right Mechanical Assembly Partner?
The right mechanical assembly partner should improve launch stability, reduce supplier complexity, and support quality from prototype through production. If a supplier only offers bench labor without upstream process understanding, they may not be equipped for complex OEM programs.
Look for these capabilities:
- Multi-process manufacturing knowledge across machining, casting, molding, stamping, welding, and finishing
- Engineering support for DFM, tolerance review, fixture logic, and assembly sequencing
- Quality systems and traceability with documented inspection and process control
- Scalable production support from prototypes to volume production
- Finishing and logistics integration for packaging, warehousing, and delivery planning
- Clear accountability across the full program, not just one assembly station
Meco applies its IATF 16949:2016-certified quality management system to assembly planning, process control and review. The inspection and documentation package for any program should still be agreed with the customer in advance.
Why Turnkey Manufacturing Improves Mechanical Assembly Outcomes
Turnkey manufacturing improves mechanical assembly because it removes gaps between design, part production, finishing, assembly, packaging, and delivery. Instead of coordinating separate suppliers for each step, OEMs work with one partner responsible for execution across the full workflow.
That improves communication speed, tolerance ownership, launch coordination, quality consistency, lead time reduction, and logistics alignment. For OEMs trying to reduce supplier count, that is often the biggest advantage.
This is the value of Meco’s turnkey manufacturing approach . It connects design support, tooling, component production, finishing, assembly, packaging, and global delivery under one accountable partner.
Conclusion
Mechanical assembly is the disciplined process of turning individual components into a finished product that performs as intended in the real world. For OEMs, it is where design intent, tolerance control, part quality, and operational discipline either come together or break down.
The strongest assembly programs do not treat assembly as an isolated labor step. They tie it to engineering review, machining, molding, coating, inspection, packaging and logistics. An integrated workflow can reduce handoff errors when products become more complex.
If your team is sourcing a new supplier, consolidating vendors, or scaling from prototype to production, Meco can support your program with integrated mechanical assembly services , whole product manufacturing , and global delivery support.
Contact Meco to discuss your drawings, materials, volumes, and timeline.
Plan Your Next Assembly
Send Meco your drawings, BOM, joining requirements and expected volumes. Our engineering team can review assembly scope alongside component production, finishing and shipment planning.
- DFM review. Joint access, fit and build sequence.
- Process scope. Machining, finishes and final assembly.
- Quality planning. Inspection records and traceability.
- Production support. Prototype through volume programs.
References and sources
- National Institute of Standards and Technology (NIST). Design for tolerance of electro-mechanical assemblies: an integrated approach . 1998.
- JTEKT Corporation. Bearing mounting and correct press-fit force application . Bearing Knowledge.
- ASTM International. ASTM B633-23: Standard Specification for Electrodeposited Coatings of Zinc on Iron and Steel . 2023.
- Defense Logistics Agency (ASSIST). MIL-PRF-8625: Anodic Coatings for Aluminum and Aluminum Alloy . Active specification record.
- Nordson. Complete Guide to Powder Coating . Background process guide.
