
How Long Does Die Casting Take?
A new die casting program typically takes 14 to 24 weeks from quote to first delivery. Tooling is the bottleneck at 4 to 12 weeks, T1 sampling adds 1 to 2 weeks, and FAI or PPAP adds another 1 to 3 weeks. The casting cycle itself takes only 20 to 60 seconds per part.
That gap between a 30-second cycle and a six-month program surprises almost every buyer the first time they see it. The casting is fast. Everything that has to happen before the first good casting is not.
Six months can be daunting, whether the launch date belongs to you, your customer, or your boss. This guide breaks down exactly where those weeks go, which ones are genuinely fixed, and which ones a turnkey partner can compress without cutting corners on die casting lead time.

How Long Does Die Casting Take From Quote to Delivery?
The full die casting timeline from quote to first delivery runs 14 to 24 weeks for a new program. That covers quoting, design-for-manufacturability review, tooling build, T1 sampling, first article inspection, pilot production, full production, and freight. Once tooling exists and the process is validated, repeat orders typically run 4 to 10 weeks.
Here is the milestone-by-milestone breakdown a sourcing manager can drop straight into a project plan.
| Milestone | What Happens | Typical Duration |
|---|---|---|
| 1. Quote and DFM Review | CAD upload, material and finish selection, DFM feedback returned | 1 to 5 business days |
| 2. PO and Engineering Sign-Off | Customer approves quote, releases PO, tool design is frozen | 1 to 2 weeks |
| 3. Tooling Build | Mold design, steel procurement, rough machining, heat treatment, finish machining, EDM, bench fitting | 4 to 12 weeks (12 to 20 for complex multi-slide) |
| 4. T0 and T1 Sampling | First shots off the new tool, dimensional checks, parameter development | 1 to 2 weeks |
| 5. FAI and PPAP (if required) | First Article Inspection, full documentation, customer approval | 1 to 3 weeks |
| 6. Pilot Run | 50 to 500 parts under production-intent conditions | 1 to 2 weeks (often overlaps with FAI) |
| 7. Full Production | Volume casting, secondary machining, finishing, packaging | 2 to 6 weeks |
| 8. Shipping and Customs | Logistics from factory to your dock | 3 days (air) to 6 weeks (sea) |
Why the Numbers Do Not Simply Add Up
If you sum those ranges end to end you get roughly 11 weeks at the absolute floor and 34 weeks at the absolute ceiling. Neither extreme happens often, and any supplier quoting you the floor is quoting you a best case that assumes nothing goes wrong.
The 11-week floor requires a simple single-cavity zinc tool, no PPAP, zero tool correction loops, and air freight. The 34-week ceiling assumes a complex multi-slide aluminum tool, a full Level 3 PPAP, heavy secondary machining and finishing, and ocean freight.
Most real programs land at 14 to 24 weeks because several stages run in parallel rather than in sequence. Fixture and gauge fabrication happens during the tool build. Packaging development and finish qualification happen during sampling. The pilot run frequently doubles as the FAI lot. When you ask a supplier for a schedule, ask specifically which stages they are overlapping, because that single question separates a real plan from a stacked-up wish list.
To see how the casting step fits into a larger manufacturing program, review Meco's die casting services overview.
Die Casting Tooling Lead Time: Why Steel Dies Take 4 to 20 Weeks
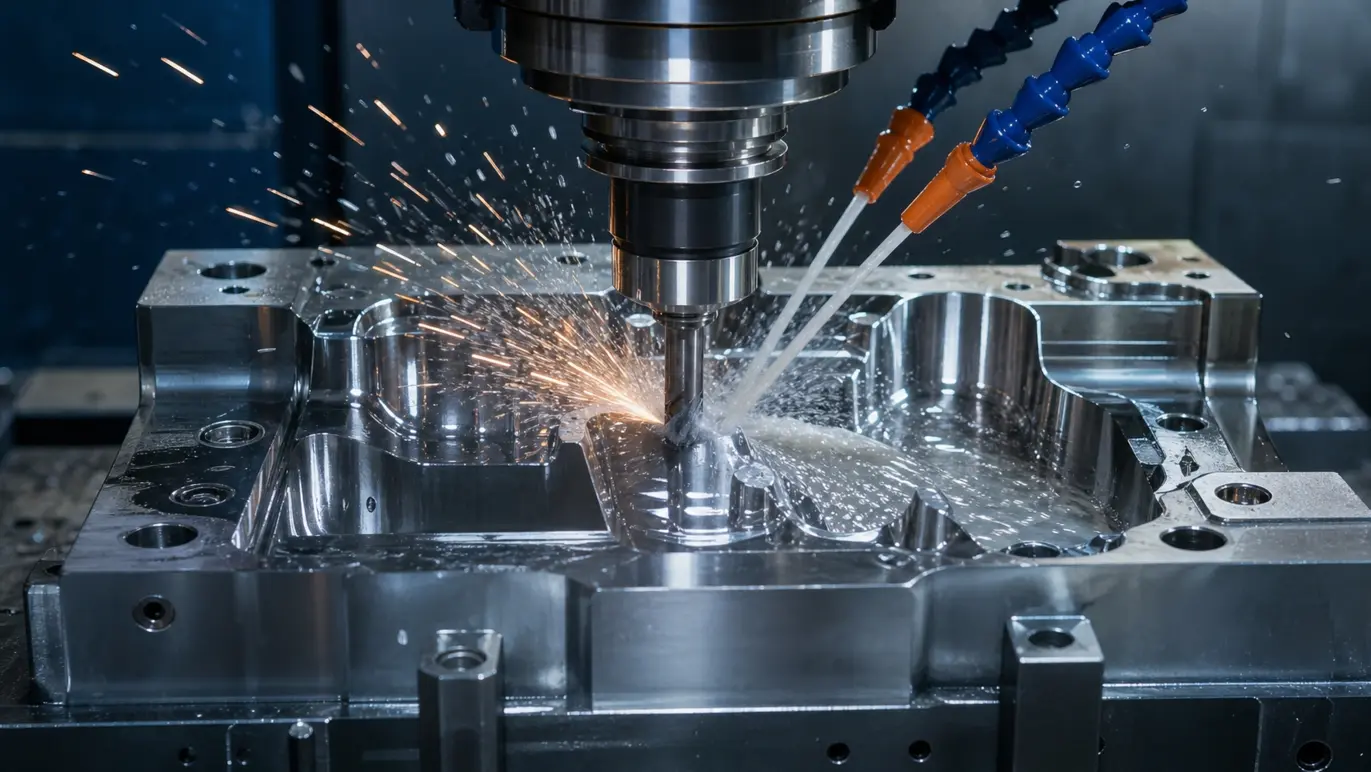
The single biggest driver of die casting lead time weeks is tooling. A high-pressure die casting die is a hardened hot-work tool steel block machined to the exact shape of your part, with conformal cooling lines, ejector pins, slides, and a gating and overflow system built in. It has to survive repeated thermal shock from molten metal injected at high velocity and intensified to thousands of PSI, so it cannot be rushed.
The Right Steel Matters, and It Affects Your Schedule
Die casting cavity steels are hot-work grades, not plastic mold steels. The workhorse is H13 (equivalent to SKD61 and DIN 1.2344), typically hardened to 44 to 48 HRC for aluminum work. Premium remelted grades such as 1.2344 ESR, DIEVAR, and QRO 90 offer better thermal fatigue resistance and can extend die life meaningfully. P20 appears in die casting too, but only in holder blocks, mold bases, and non-contact components, never in the cavity itself.
Steel choice is a schedule decision as well as a quality decision. Standard H13 is usually on the shelf and available in days. Premium ESR and specialty grades can add 10 to 15 days of procurement, which is often worth trading for 30 to 50 percent more tool life on a high-volume program.
What Goes Into Building a Die Casting Mold
The die casting mold lead time breaks down into eight steps. The one most online guides omit is heat treatment, and it is a real fixed block of calendar time that cannot be compressed.
- Mold design and flow simulation: 3 to 7 days. Engineers model the cavity, gating, runners, and overflows, then run simulation to predict fill pattern, air entrapment, porosity, and shrinkage.
- Steel procurement and block prep: 3 to 10 days. Tool steel is sourced, cut, and squared. Premium grades extend this.
- Rough machining: 3 to 5 days. The cavity is roughed out with stock left on for post-heat-treat finishing.
- Vacuum heat treatment: 4 to 6 days. Hardening, quenching, and multiple temper cycles bring the steel to 44 to 48 HRC. This is a furnace-scheduled operation, usually at an outside processor, and it does not shorten no matter how much you pay.
- Finish machining, EDM, and polishing: 7 to 12 days. Final cavity geometry is cut into hardened steel using precision CNC and electrical discharge machining, then polished to the required surface finish.
- Optional surface treatment: 2 to 4 days. Nitriding or PVD coating for soldering resistance and extended die life.
- Assembly and bench fitting: 4 to 6 days. Ejector pins, slides, cores, and inserts are installed and hand-fitted.
- T0 and T1 trial shots plus corrections: 3 to 5 days. The die runs its first shots and issues are corrected.
That is the standard path for a conventional tool. Parts with multiple hydraulic slides, deep undercuts, or multi-cavity layouts push past 12 weeks and can reach 20.
Bridge Tooling vs Production Tooling: When You Can Cut the Timeline
If your program is on the clock, there are faster paths. Bridge tooling for high-pressure die casting does not mean an aluminum die, which will not survive molten aluminum at roughly 660 degrees Celsius. It means a simplified steel tool: a standardized mold base, a single cavity, pre-hardened or unhardened steel, hand-loaded inserts instead of hydraulic slides, and a reduced cooling circuit. You give up cycle time and tool life, and you get parts weeks earlier.
| Tooling Type | Lead Time | Practical Shot Capacity | Best For |
|---|---|---|---|
| Bridge Tool (soft or pre-hardened steel, standard base) | 2 to 4 weeks | 5,000 to 50,000 | Market validation, bridge production, fast launch |
| Standard Single-Cavity Hardened Steel | 4 to 8 weeks | Alloy dependent (see table below) | Medium to high volume, stable design |
| Multi-Cavity Hardened Steel | 8 to 12 weeks | Alloy dependent, per cavity | High volume, cost-per-part optimized |
| Complex Multi-Slide Hardened Steel | 12 to 20 weeks | Alloy dependent, slides wear first | Undercuts, side actions, complex geometry |
Die Life Is Driven by Alloy, Not Cavity Count
A common misconception is that multi-cavity tools last longer. They do not. Cavity count multiplies parts per shot, but every cavity sees the same thermal cycle, so the die does not gain life. What actually governs die life is the alloy being cast, because thermal load is what kills tool steel.
| Alloy | Approx. Melt Temperature | Typical Die Life (Shots) | Typical Cycle Time |
|---|---|---|---|
| Zinc (Zamak 3, Zamak 5) | Around 390 to 420 °C | 500,000 to 1,000,000+ | 15 to 30 seconds |
| Magnesium (AZ91D) | Around 650 °C | 100,000 to 200,000 | 20 to 40 seconds |
| Aluminum (A380, ADC12, A360) | Around 660 to 700 °C | 100,000 to 150,000 typical, up to 200,000 with premium steel | 30 to 60 seconds |
| Brass and Copper | Around 900 to 1,000 °C | 10,000 to 50,000 | 40 to 90 seconds |
These are planning figures consistent with NADCA industry guidance. Actual life varies significantly with steel grade, heat treatment quality, thermal management, die spray practice, and preventive maintenance discipline. Budget for a spare cavity insert on any aluminum program expected to exceed 150,000 shots, and order it during the original tool build rather than after the first one cracks.
What Die Casting Tooling Costs and How That Affects Your Schedule
Tooling cost and tooling lead time move together, so it helps to see both. These are indicative US-facing market ranges for planning purposes only; your actual quote depends on part size, geometry, cavity count, and slide complexity.
| Tool Type | Indicative Cost Range | Lead Time |
|---|---|---|
| Bridge tool, small simple part | $3,000 to $12,000 | 2 to 4 weeks |
| Single-cavity steel, small part | $8,000 to $25,000 | 4 to 8 weeks |
| Single-cavity steel, medium part with slides | $20,000 to $50,000 | 6 to 10 weeks |
| Multi-cavity steel | $40,000 to $100,000 | 8 to 12 weeks |
| Large or complex multi-slide | $80,000 to $200,000+ | 12 to 20 weeks |
The amortization math is what should drive the decision. A $60,000 tool spread over 5,000 parts adds $12.00 per part. The same tool over 200,000 parts adds $0.30. If your annual volume is genuinely uncertain, a bridge tool that gets you to market in four weeks and lets you confirm demand before committing to a production die is often the cheaper path overall, even though you pay for tooling twice.
Want a tooling timeline and cost mapped to your specific part? Send the CAD to Meco's engineering team and you will get DFM feedback inside 24 hours.
What Is T1 Sampling and How Long Does It Take?
T1 sampling is the first set of parts produced from a brand-new tool. The T stands for trial and the 1 means it is the first round. T1 parts get measured, inspected, and compared against your drawings. If they pass, the tool moves toward production. If they do not, the tool goes back for correction.
Quick Definition: T0, T1, T2
T0 is the very first shot off a new die, run mainly to confirm the tool opens, closes, fills, and ejects without damage. Parts are often scrap. T1 is the first sample round expected to match the design, and it is what gets measured and reported. T2 and T3 are correction rounds after tool modifications. Most well-engineered programs reach approval at T1 or T2; a program that reaches T4 usually had a DFM problem that was never caught on paper.
Time to First Sample After Tool Completion
Once the tool is built and assembled, time to first sample is usually 3 to 7 working days. The die is mounted on a machine of the correct clamping tonnage, the alloy is brought to temperature, shot profile and intensification pressure are dialed in, die spray is set, and the first parts come off. Engineers measure them on a CMM and issue a dimensional report.
If the part meets spec on the first attempt, you are ahead of schedule. In practice most programs need one or two correction loops, and each loop adds 1 to 3 weeks depending on whether the fix is a parameter change, a weld-and-recut, or a new insert. Meco's R&D engineering team runs mold flow simulation before any steel is cut, which moves most of those discoveries from the shop floor to the screen.
First Article Inspection and PPAP Timing
For programs requiring formal quality documentation, the next step is die casting first article inspection (FAI) and, in automotive, the full Production Part Approval Process (PPAP). FAI is a complete dimensional report on the first production-intent parts. PPAP bundles FAI together with material certificates, control plans, PFMEA, MSA, and initial SPC data into a package your customer signs off on.
FAI typically takes 5 to 10 working days. A full Level 3 PPAP can take 2 to 3 weeks. These steps follow the APQP framework defined by the Automotive Industry Action Group (AIAG), the standard playbook for IATF 16949 certified manufacturers like Meco.
One scheduling trap worth naming: PPAP approval is a two-sided process. The supplier submits, but the clock keeps running while your own quality team reviews. Buyer review time is one of the most commonly underestimated blocks in the whole timeline. Agree on a review turnaround commitment up front and put it in the project plan alongside the supplier milestones.
Die Casting Cycle Time: How Long Does One Shot Take?
Die casting cycle time is the time to produce one shot, measured from the moment the die closes to the moment it is ready to close again. Typical cycles run 20 to 60 seconds, depending on part size, wall thickness, alloy, and thermal management.
Here is where those seconds go on a conventional cold-chamber aluminum machine.
| Cycle Stage | What Is Happening | Typical Duration |
|---|---|---|
| 1. Die Close and Lock | Die halves come together through fast, low-pressure, then high-pressure clamping | 1.5 to 3 seconds |
| 2. Metal Delivery | Molten alloy is ladled into the shot sleeve (cold chamber only) | 2 to 4 seconds |
| 3. Injection and Cavity Fill | Slow shot clears the sleeve, then the plunger accelerates and fills the cavity | Fill itself is 0.02 to 0.1 seconds |
| 4. Intensification and Pressure Hold | Pressure is intensified to feed shrinkage and reduce porosity | 1 to 5 seconds |
| 5. Cooling and Solidification | Metal solidifies to ejection strength inside the die | 5 to 30 seconds |
| 6. Die Open and Ejection | Die opens, ejector plate pushes the casting out, part is extracted | 1 to 3 seconds |
| 7. Die Spray and Blow-Off | Release agent applied, cavity cooled and cleared for the next shot | 2 to 5 seconds |
Why Cooling and Die Spray Dominate the Cycle
Cooling alone is typically more than half the cycle. The metal has to solidify enough to hold its shape and survive ejection, or the part distorts, sticks, or tears. Thicker walls take disproportionately longer to cool, because solidification time scales roughly with the square of section thickness. Higher-melting alloys like aluminum take longer than zinc.
Die spray is the second most underrated block. It is doing two jobs at once, applying release agent and pulling heat out of the die surface, and a poorly balanced cooling circuit forces operators to spray longer to compensate. Good conformal cooling design in the tool buys back seconds on every shot for the life of the program.
This is why DFM matters so much. Reducing a 4 mm wall to 2.5 mm where the application allows can cut solidification time substantially, which cuts your die casting production time, your cost per part, and your thermal load on the die all at once. For more on the process itself, see what is die casting.
What Cycle Time Means in Actual Output
Let us do the arithmetic, because vague claims about volume are easy to make and easy to check. At a 30-second cycle, a single-cavity tool running 24 hours produces about 2,880 shots. Applying a realistic 85 percent overall equipment effectiveness gives roughly 2,400 good parts per machine per day. A four-cavity tool on the same cycle yields around 9,500 parts per day.
So the honest statement is thousands of parts per day per machine, scaling with cavity count and machine count. That is still extraordinarily fast compared to machining or additive, and it is why die casting wins on high-volume programs despite the tooling investment up front.
Die Casting Production Time: Pilot Run to Full Volume
Once T1 and FAI are approved, you move into pilot production, then full volume. Pilot runs are usually 50 to 500 parts, used to validate the process under near-production conditions, prove out fixtures and gauges, and confirm that secondary operations hold. They typically take 1 to 2 weeks including inspection.
Full production timing depends on quantity, secondary operations, and finishing. A 10,000-piece order of a simple aluminum bracket with no machining or coating might take 1 to 2 weeks of pure casting. The same order with CNC post-machining and powder coating can stretch to 4 to 6 weeks, because parts have to flow through multiple stations, each with its own queue.
Finishing is where outsourced supply chains quietly lose time. Anodizing, e-coating, powder coat, chromate, and plating are frequently subcontracted, and each handoff adds transit plus queue plus a return inspection. Two to three outside finishing vendors on one part number can add three weeks to a job that casts in four days.
First Production Run vs Repeat Run: The Insight Most Buyers Miss
Here is something competitors rarely put in writing. The first production run of a brand-new part can take up to 24 weeks from quote to dock, because every step has to happen for the first time. Repeat runs of the same part typically come in at 4 to 10 weeks, including ocean freight.
The reason is simple. The tool exists. The shot profile and thermal settings are recorded. The DFM is done. The fixtures and gauges are built. The PPAP package is signed. What remains is scheduling, raw material, casting, finishing, inspection, and shipping. If you are planning a product that will reorder repeatedly, the repeat-run number is the one that belongs in your inventory model from the second order onward.
Two caveats keep that number honest. A previous ship date does not guarantee the next one if the drawing revision changed, the tool needs refurbishment, the alloy is on allocation, or machine capacity is committed elsewhere. And a tool that has been sitting idle for a year needs condition assessment before it runs. Ask for tool condition and remaining shot estimate at the time you place a repeat PO, not after.
Prototype Routes Before You Cut a Production Die
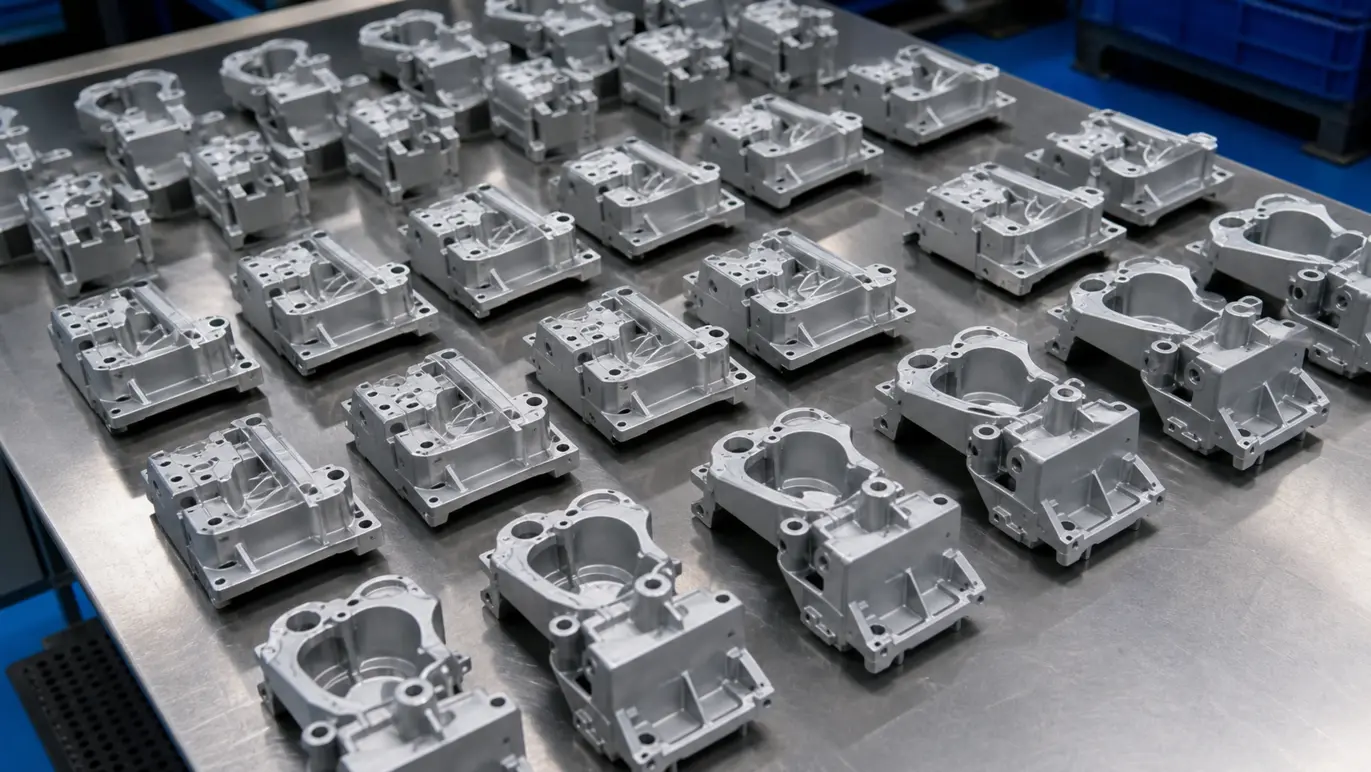
If your design is not fully locked, cutting a production die is the most expensive way to discover that. Prototyping first adds weeks on paper but usually saves weeks in reality, because a mid-tooling design change costs far more calendar time than a prototype round.
The critical question with any prototype is not how fast it arrives but what it actually proves.
| Prototype Route | Lead Time | What It Validates | What It Does Not Validate |
|---|---|---|---|
| 3D printed polymer | 2 to 5 days | Form, fit, ergonomics, assembly clearance | Anything mechanical, thermal, or castability related |
| CNC machined from billet | 5 to 10 days | Fit, function, machined feature accuracy, wrought material strength | As-cast surface, draft, porosity, shrinkage, cast grain structure |
| Metal 3D print (DMLS or binder jet) | 5 to 15 days | Complex geometry, internal channels, functional testing | Die cast microstructure, porosity behavior, real cost signal |
| Gravity or sand cast | 2 to 4 weeks | Cast geometry, approximate cast properties, wall feasibility | HPDC-specific fill behavior, tolerances, surface finish |
| Bridge die (soft steel tool) | 2 to 4 weeks | Actual HPDC process, near-production parts, real porosity and tolerance data | Long-run process stability and final cycle time |
The practical rule: use CNC or printing to validate geometry and assembly, and use a bridge die when you need parts that behave like die castings. A machined billet prototype will pass a pressure test that a real casting might fail, which is exactly the kind of surprise you do not want at PPAP.
Transferring an Existing Die: The 4 to 6 Week Shortcut
If you already own a die and you are changing suppliers, you do not start the tooling clock over. Tool transfer is the single fastest way to compress a die casting program, and it is routinely overlooked because most lead-time content assumes you are starting from zero.
A transfer skips 4 to 6 weeks of tool build. Budget roughly 2 weeks for assessment and refit at the receiving plant, plus transit. Total time to first parts is usually 4 to 8 weeks rather than 14 to 20.
What the receiving plant has to verify before it runs your die:
- Machine compatibility. Clamping tonnage, tie-bar spacing, platen size, shot sleeve diameter and position, and ejector stroke and pattern all have to match an available machine.
- Tool condition. Cavity wear, heat checking, soldering, parting line condition, slide wear, and remaining shot estimate. Expect a written condition report.
- Circuit compatibility. Cooling line fittings, hydraulic slide circuits, and any sensor or thermocouple provisions.
- Documentation. 3D and 2D tool data, part drawings at the current revision, last known process parameters, spare insert inventory, and prior inspection reports.
- Ownership and legal. Written confirmation that the tool is yours, tooling release from the incumbent supplier, and export documentation if the die crosses a border.
The most common failure mode is not technical, it is commercial. Incumbent suppliers sometimes delay tool release. Start that conversation before you plan the transfer date, and make sure your original tooling purchase order clearly assigned ownership.
Plan Around the Manufacturing Calendar
Calendar risk causes more blown launch dates than any engineering issue, and almost no lead-time guide mentions it.
Chinese New Year is the big one. Factories across China typically run 15 to 20 days down, and the effective disruption is longer than the official holiday because output tapers in the two weeks before as workers travel, and ramps slowly for two to three weeks after as staff return. Shipping capacity tightens sharply in the pre-holiday rush and rates spike. Chinese New Year falls in late January or February depending on the year, so confirm the exact dates for your program year.
The practical planning rule: if tooling is not released by roughly mid-December, do not plan on T1 samples before the holiday. Either release earlier, or accept a post-holiday sampling date and build it into your schedule honestly rather than discovering it in February.
Other dates that matter: Golden Week in early October, roughly a week of reduced output across China; Golden Week and Obon in Japan; Songkran in mid-April in Thailand; and the US and European summer shutdown period, which affects customer-side approvals as much as production. A PPAP submitted the week your customer's quality team goes on holiday sits in a queue regardless of how fast the supplier was.
Shipping, Tariffs, and Why Warehousing Changes the Real Number
Freight is the last leg, and it is where a program that was on schedule for five months can lose a month.
Ocean freight from Asia to the US West Coast runs roughly 18 to 30 days on the water, and 30 to 45 days to the East Coast, before you add port congestion, drayage, and inland transit. Air freight is 3 to 7 days door to door but typically costs 8 to 12 times more per kilogram, which is painful for metal castings specifically because they are dense. A common compromise is to air-ship 20 to 30 percent of the first lot to support launch and pilot builds, and put the balance on the water.
Customs and Tariff Timing
For US importers, aluminum and aluminum derivative articles fall under Section 232, and the applicable rates and the scope of covered derivative products have changed several times in recent years. Verify the current rate and classification with your customs broker before you build a landed-cost model, because published figures go stale quickly.
From a pure timeline perspective, the thing to manage is not the rate but the paperwork. Delays come from HTS classification disputes, missing country-of-origin or mill certification documentation, incomplete aluminum smelt-and-cast origin reporting where required, and CBP examination holds. A misclassified shipment can sit for one to three weeks. Confirm HTS codes and origin documentation during the PPAP phase, not when the container is already on the water.
How US and Regional Warehousing Removes Weeks From Your Lead Time
This is the lever that changes the math most, and it is one that a pure overseas supplier cannot offer you.
When finished goods are held in a domestic warehouse under a VMI or consignment program, your order-to-dock time stops being a function of ocean transit. The 4 to 6 weeks of freight and customs happen against a forecast, not against your purchase order. A release against warehoused stock ships in days.
Meco holds inventory in Ohio and Florida in the US, plus Canada, Tokyo and Osaka in Japan, and Thailand, with JIT and VMI programs available. For a customer running steady monthly volume, this turns a nominal 8-week repeat lead time into a 2-to-5 day release, while the replenishment pipeline runs continuously in the background. It does require a rolling forecast, which is a fair trade for removing an ocean crossing from your critical path.
How to Compress Your Die Casting Lead Time
If your timeline is tight, you have real options. Most of them depend on choices made before the PO is signed, so the earlier you bring your manufacturing partner into the conversation, the more weeks you save.
The 5-Lever Compression Playbook
1. Get DFM feedback before final drawings. A 30-minute design review can flag draft angles, wall thickness, parting line placement, and gating issues that would otherwise surface at T1 and trigger tool rework. That single move can save 2 to 4 weeks.
2. Use a bridge die for early volume. A simplified soft-steel tool can deliver real die cast parts in 2 to 4 weeks. Start the production die in parallel and cut over when it is ready.
3. Run mold flow simulation before cutting steel. Simulation catches air entrapment, cold shuts, and shrinkage porosity on the screen. T1 approval rates climb and correction loops drop.
4. Pick a partner with in-house secondary operations. When casting, CNC machining, heat treatment, and finishing all happen under one roof, you skip the transit, queue, and re-inspection that each external handoff adds. Meco's vertical integration of CNC machining and finishing inside the casting facility is built around exactly this.
5. Lock the design before tooling kicks off. Mid-tooling design changes are the single biggest cause of blown timelines. If your spec is still moving, delay tooling start and validate with prototypes first.
What Compression Actually Costs
Every lever above has a price, and a supplier who tells you otherwise is not being straight with you. Knowing the cost lets you spend money where it buys the most calendar.
| Compression Lever | Time Saved | Typical Cost Impact |
|---|---|---|
| Early DFM review before drawings are frozen | 2 to 4 weeks | Usually free with a serious supplier |
| Mold flow simulation before cutting steel | 1 to 3 weeks of avoided rework | Often bundled into tooling cost |
| Tooling expedite (overtime, priority scheduling) | 1 to 3 weeks | 15 to 30 percent tooling premium |
| Bridge die run in parallel with production die | 6 to 8 weeks to first parts | Full cost of a second, simpler tool |
| Capacity reservation on the machine | 1 to 3 weeks of queue | Commitment or deposit, commonly 10 to 15 percent |
| Partial air freight on first lot | 4 to 6 weeks on that portion | 8 to 12x sea freight cost per kg |
| Domestic VMI stock on repeat orders | 4 to 6 weeks per order | Inventory carrying cost plus forecast commitment |
Note what is not on this list: skipping FAI, shortening heat treatment, or reducing T1 inspection. Those are not compression, they are risk transfer, and they reliably cost more weeks later than they save now.
Why Lead Times Vary: 7 Factors That Shift the Timeline
Two die casting programs that look similar on paper can have lead times eight weeks apart. Here is what usually causes the gap:
- Part complexity. Undercuts, hydraulic slides, thin walls, and tight flatness requirements add tool design time, machining time, and correction loops.
- Alloy choice. Zinc tools build faster, run shorter cycles, and last far longer. Aluminum demands more robust tooling, better thermal management, and longer cooling.
- Cavity count. Multi-cavity tools take longer to build and require balanced runner design, but cut cost per part substantially at volume.
- Secondary operations. CNC machining, heat treatment, impregnation, and surface finishing each add queue time, and outsourced finishing adds transit on top.
- Quality requirements. Full Level 3 PPAP for automotive adds 2 to 3 weeks over a simple industrial FAI, plus buyer review time.
- Material availability. Standard A380 and ADC12 are readily available. Specialty or high-conductivity alloys can add 1 to 3 weeks of procurement.
- Shipping route and customs. Sea freight is 4 to 6 weeks door to door. Air is days at 8 to 12x the cost. Classification or documentation issues can add 1 to 3 weeks at the border.
For deeper context on how all this rolls up into a full program, see Meco's whole product manufacturing approach, built for OEMs that want one accountable partner from quote to global delivery. If you are still evaluating whether to outsource at all, this guide to contract manufacturing walks through the tradeoffs.
Bottom line: a typical new die casting program runs 14 to 24 weeks from quote to dock. The biggest block is tooling, which you can compress with a bridge die or, better, by avoiding rework through up-front DFM and simulation. Once the tool exists, repeat runs come in at 4 to 10 weeks, and domestic warehoused stock brings that down to days. Plan for the first one, scale on the second.
Frequently Asked Questions About Die Casting Lead Time
How long does die casting take from quote to delivery?
A new die casting program typically takes 14 to 24 weeks from quote to first delivery. Tooling consumes 4 to 12 weeks, T1 sampling adds 1 to 2 weeks, FAI or PPAP adds another 1 to 3 weeks, and full production plus shipping adds 3 to 10 weeks. Once tooling exists and the process is validated, repeat orders of the same part typically run 4 to 10 weeks including ocean freight.
How long does it take to make a die casting mold?
A standard single-cavity hardened steel die casting mold takes 4 to 8 weeks to build. Multi-cavity steel tools run 8 to 12 weeks, and complex tools with multiple slides or undercuts can stretch to 12 to 20 weeks. A simplified bridge die in soft or pre-hardened steel can be ready in 2 to 4 weeks if you accept a shorter shot capacity of 5,000 to 50,000 parts.
What is die casting cycle time?
Die casting cycle time is the time it takes to produce one shot, from the moment the die closes to the moment it is ready to close again. Typical cycles run 20 to 60 seconds. Cooling and solidification account for more than half that time, usually 5 to 30 seconds, because the metal has to harden enough to survive ejection before the die opens.
How many parts can a die casting machine produce per day?
At a 30-second cycle, a single-cavity tool produces about 2,880 shots in 24 hours, or roughly 2,400 good parts after accounting for realistic machine availability. A four-cavity tool on the same cycle yields around 9,500 parts per day. Output scales with cavity count and machine count, so high-volume programs run thousands of parts per day per machine.
What is a T1 sample in die casting?
A T1 sample is the first set of parts produced from a brand-new die casting mold that is expected to match the design. The T stands for trial. Engineers measure these parts on a CMM and compare them against the drawings. If they pass, the tool moves toward production. If they do not, the tool goes back for correction, which usually adds 1 to 3 weeks for each loop.
How long does aluminum die casting take vs zinc die casting?
Zinc die casting is faster than aluminum at almost every step. Zinc tools are simpler to build, and zinc melts at around 390 to 420 degrees Celsius versus roughly 660 for aluminum, which means shorter cooling and faster cycle times of 15 to 30 seconds against 30 to 60 seconds. Zinc dies also last far longer, commonly 500,000 to over 1,000,000 shots compared to 100,000 to 150,000 for aluminum.
Why is die casting tooling lead time so long?
Die casting dies are built from hot-work tool steel such as H13, SKD61, or 1.2344 and must survive repeated thermal shock from molten metal injected at high velocity and pressure. The build includes mold design and simulation, steel procurement, rough machining, vacuum heat treatment to 44 to 48 HRC, finish machining and EDM in hardened steel, hand fitting of ejector pins and slides, and trial shots. Heat treatment alone is a furnace-scheduled 4 to 6 days that cannot be rushed.
Can rapid or bridge tooling really cut die casting lead time?
Yes, but not by using aluminum dies, which will not survive molten aluminum. Bridge tooling for high-pressure die casting means a simplified steel tool with a standardized mold base, a single cavity, pre-hardened or unhardened steel, and hand-loaded inserts instead of hydraulic slides. That can deliver real die cast parts in 2 to 4 weeks instead of 4 to 12, with a practical capacity of 5,000 to 50,000 shots.
How long is the first article inspection for a die casting?
A standard First Article Inspection for a die cast part typically takes 5 to 10 working days, including full dimensional measurement on a CMM, visual inspection, and the report itself. A full Level 3 PPAP package, required in automotive and some aerospace programs, can take 2 to 3 weeks because it bundles FAI with material certificates, control plans, PFMEA, MSA, and initial SPC data. Buyer review time runs on top of that and is commonly underestimated.
What is the lead time difference between the first production run and repeat runs?
First production runs can take up to 24 weeks because every step happens for the first time, including tooling, DFM, T1, FAI, and PPAP. Repeat runs of the same part typically come in at 4 to 10 weeks including ocean freight, because the tool exists and the process is validated. With domestic warehoused stock under a VMI program, a release can ship in days instead of weeks.
Can I transfer an existing die casting tool to a new supplier?
Yes, and it is the fastest way to compress a program. A tool transfer skips 4 to 6 weeks of die build, leaving about 2 weeks for condition assessment and refit plus transit, so first parts usually land in 4 to 8 weeks rather than 14 to 20. The receiving plant must verify clamping tonnage, tie-bar spacing, shot sleeve and ejector compatibility, cooling and hydraulic circuits, and tool condition. Confirm written tool ownership and get a tooling release from the incumbent before scheduling the move.
How does Chinese New Year affect die casting lead times?
Factories across China typically run 15 to 20 days down for Chinese New Year, but the real disruption is longer because output tapers for about two weeks before as workers travel and ramps slowly for two to three weeks after. Freight capacity tightens and rates spike in the pre-holiday rush. As a planning rule, tooling released after roughly mid-December will not produce T1 samples before the holiday, so either release earlier or build the post-holiday date into your schedule.
How much does it cost to expedite a die casting order?
Tooling expedite through overtime and priority scheduling typically carries a 15 to 30 percent premium and saves 1 to 3 weeks. Reserving machine capacity usually requires a commitment or deposit of around 10 to 15 percent and removes 1 to 3 weeks of queue. Air freight costs roughly 8 to 12 times sea freight per kilogram and saves 4 to 6 weeks. Early DFM review and mold flow simulation are usually free or bundled, and they save the most calendar time of any lever.
Does US warehousing reduce die casting lead time?
Yes, significantly, because it removes ocean transit and customs from your critical path. When finished goods are held domestically under a VMI or consignment program, the 4 to 6 weeks of freight happen against a forecast rather than against your purchase order, and a release ships in days. The trade-off is a rolling forecast commitment and inventory carrying cost. Meco holds stock in Ohio and Florida, plus Canada, Japan, and Thailand.
Need Die Cast Parts Delivered On Schedule? Let's Map Your Timeline.
Most die casting delays come from fragmented suppliers, late DFM feedback, and handoffs between separate vendors for casting, machining, and finishing. Meco eliminates all three. We own the tooling, casting, machining, finishing, and assembly steps under one roof, with U.S. engineering support and global warehousing.
With 30+ years of turnkey manufacturing experience and IATF 16949:2016 certified quality, Meco is built for OEM programs where the launch date is fixed and the timeline is tight.
- 24-Hour Quote with DFM Feedback: Most lead-time problems get fixed before tooling starts.
- In-House Tooling: Standard single-cavity steel dies in 4 to 8 weeks. Bridge tooling available in 2 to 4 weeks for early volume.
- 40+ Processes Under One Roof: Die casting, CNC machining, heat treatment, surface finishing, and assembly. No handoff delays.
- IATF 16949:2016 Certified: Full APQP and PPAP support, with control plans, PFMEA, MSA, and SPC documentation handled in house.
- Global Logistics: Warehousing in the U.S. (Ohio and Florida), Canada, Japan (Tokyo and Osaka), and Thailand. JIT and VMI programs turn a multi-week repeat order into a multi-day release.
Send your drawings and let Meco's engineering team show you exactly where the weeks go, and where they can be saved.
Request a Quote Today